Why Choose Contract Softgel Manufacturing? The question matters as supplement and pharmaceutical brands face tighter quality expectations, shorter launch windows, and rising equipment costs. Grand View Research estimates that the global softgel capsules market will continue expanding through 2030, supported by demand for convenient, easy-to-swallow dosage forms. Its analysis also identifies contract manufacturing as an important route for improving production flexibility.
Contract Softgel Manufacturing gives companies access to encapsulation lines, gelatin preparation systems, stability testing, and experienced quality teams. A capable partner can manage formulation trials, fill-weight control, leak testing, packaging, and batch documentation under one system. The practical difference appears on the factory floor. Operators check capsule seams, inspect transparent shells, and remove units with visible defects before release.
Former FDA official Dr. Janet Woodcock stated, “Quality cannot be tested into products; it has to be built into them.” That principle is highly relevant to softgel production. It supports supplier audits, validated processes, traceable raw materials, and scientifically justified specifications. It also demands honest communication.
Outsourcing is not automatically cheaper. A weak partner may create delays, transfer problems, or inconsistent batches. That risk deserves attention. A 2023 MarketsandMarkets report describes the pharmaceutical contract manufacturing market as increasingly driven by outsourcing, specialized capacity, and development efficiency. Still, market growth does not guarantee supplier quality.
The strongest decision compares technical capability, regulatory experience, minimum order quantities, lead times, and communication standards. Brands should request evidence, not promises. A well-chosen manufacturer can turn a complex softgel concept into a consistent, commercially realistic product. But careful due diligence remains essential.
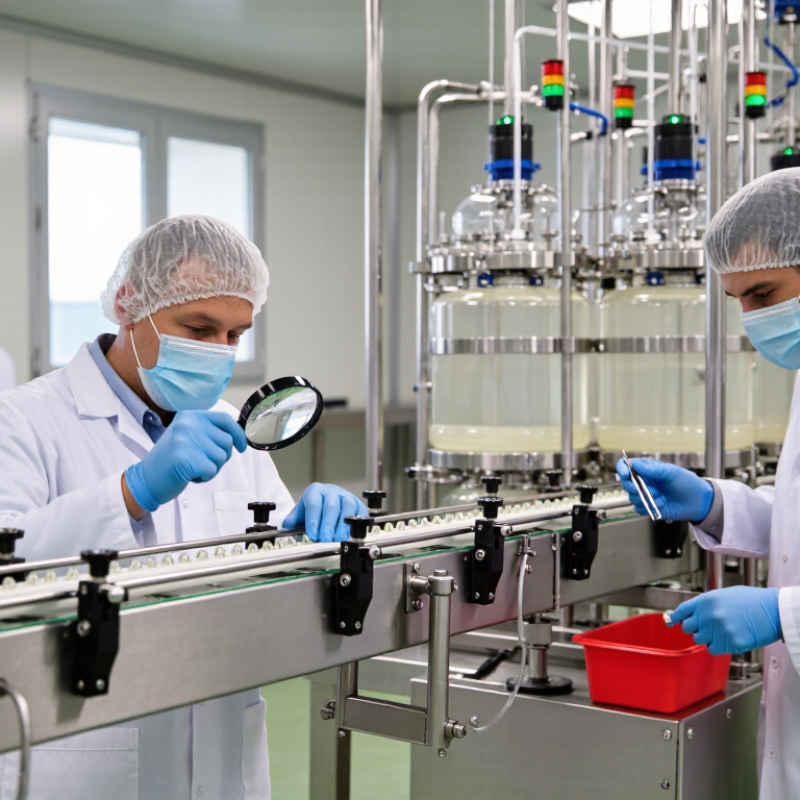
Contract softgel manufacturing means hiring a qualified specialist to manage production under your specifications. The process may include formulation, raw-material sourcing, encapsulation, testing, packaging, and batch documentation. A typical facility checks fill weight, seam integrity, shell moisture, potency, dissolution, and microbial limits. These details matter when a capsule must remain stable in a bottle, warehouse, or warm delivery truck.
The model can reduce capital pressure. You may avoid purchasing encapsulation machines, installing controlled rooms, and building an in-house quality team. Grand View Research valued the global dietary supplements market at approximately USD 177.5 billion in 2023. Its report also projects strong growth through 2030. Demand is rising, but growth does not excuse weak controls. The Council for Responsible Nutrition’s 2024 consumer survey reported that roughly three-quarters of U.S. adults use dietary supplements. Consumers still expect consistency.
A reliable partner should provide documented GMP procedures, supplier qualification, laboratory testing, and traceable batch records. Ask how deviations are investigated. Ask who approves release results. Ask about stability studies, too. Softgels are sensitive to heat, oxygen, and formulation changes. The process is not a shortcut. A poor specification can still produce a poor batch. Even experienced teams sometimes revise fill viscosity, shell composition, or packaging after stability data reveals an unexpected change. That learning is part of responsible manufacturing.
It may cover formulation, ingredient sourcing, encapsulation, testing, packaging, and batch documentation. A facility may also monitor fill weight, seam integrity, potency, moisture, dissolution, and microbial quality.
Outsourcing can reduce equipment costs and avoid building controlled rooms or an internal quality team. It also provides trained operators and specialized production equipment. The savings are not automatic.
Technical staff review the active ingredients, dosage, capsule size, viscosity, and stability needs. Small laboratory batches test whether the fill moves evenly. Sometimes, the first trial fails.
The fill may leak, settle, or become too thick. The shell may dry unevenly. These results reveal needed changes before larger production. Failure can teach something useful.
Rotary dies shape the shell, add the liquid fill, and seal each capsule. Operators monitor temperature, weight variation, sealing quality, and production speed. The capsules then enter drying tunnels.
Testing may confirm identity, potency, appearance, dissolution, moisture, and microbial limits. Facilities should record results for traceability. Batch records support release decisions.
Suitable formats can include bottles, blister packs, or other protective containers. Packaging should suit the product’s sensitivity to heat, oxygen, and moisture. A warm delivery truck can matter.
Ask about documented quality procedures, supplier qualification, laboratory testing, stability studies, and deviation investigations. Also ask who approves batch release. Communication deserves careful review.
No. The product owner still needs written specifications, testing expectations, supplier requirements, and change-control procedures. Regular reviews help maintain consistency. Mistakes still happen.
Contract Softgel Manufacturing is a strategic way for companies to develop and produce softgel supplements without building and managing their own production facilities. In this arrangement, a specialized manufacturer supports the project from formulation and ingredient sourcing to encapsulation, packaging, and final delivery. The process typically includes product planning, formulation review, raw material testing, pilot production, quality inspections, and large-scale manufacturing, helping ensure consistent results at every stage.
Outsourcing softgel production can reduce investment in equipment, improve operational efficiency, and provide access to technical expertise and flexible production capacity. However, quality and safety should remain top priorities. Businesses should evaluate a manufacturer’s quality management systems, regulatory compliance, testing procedures, facility standards, documentation, and ability to maintain batch-to-batch consistency. The right partner should also communicate clearly, protect product specifications, offer reliable lead times, and demonstrate experience with the intended product category. A careful selection process can support efficient development, dependable quality, and long-term business growth.

