
Film-Coated Multivitamins
High-potency multi-nutrient complexes featuring aqueous film coating to eliminate odor, shield against oxidation, and ensure smooth swallowing.
Pharmaceutical-grade custom tablet formulation, direct compression, advanced film coating, and turnkey packaging — engineered in Scarborough, Canada for global supplement brands.
Selecting a partner for your Vitamin Tablet Manufacturing Service requires far more than comparing per-unit press costs. In today's highly regulated global nutraceutical market, brand equity depends on batch-to-batch content uniformity, rapid disintegration, friability resistance, and verifiable regulatory clearance. NutraLab Canada Corp. operates a state-of-the-art Health Canada site-licensed contract manufacturing facility located at 980 Tapscott Rd, Scarborough, Ontario, delivering pharmaceutical-grade tablet manufacturing services tailored to corporate importers, pharmacy retail chains, practitioner brands, and fast-growing direct-to-consumer supplement enterprises.
Our formulation scientists and process engineers bring over two decades of hands-on experience in particle engineering, powder rheology, moisture protection, and high-speed rotary compression. Whether your brand requires high-potency multivitamin tablets, bioavailable chelated mineral complexes, chewable botanical tablets, or specialized modified-release delivery systems, NutraLab manages the complete product lifecycle under one unified Quality Management System (QMS).
From classic daily multivitamins to complex multi-phase kinetic release formulations, our end-to-end vitamin tablet manufacturing service offers versatile delivery formats optimized for bioavailability, stability, and consumer swallowability.
High-potency multi-nutrient complexes featuring aqueous film coating to eliminate odor, shield against oxidation, and ensure smooth swallowing.
Palatable, flavor-masked chewable tablets and orally disintegrating tablets (ODTs) designed for pediatric, senior, and pill-averse consumer segments.
Time-release hydrophilic matrix tablets and acid-resistant enteric coatings that deliver active vitamins continuously over 6 to 12 hours.
Rapidly dissolving sublingual tablets and effervescent formulations engineered for fast mucosal absorption and superior active bioavailability.
100% plant-based tablet formulations utilizing organic acacia, organic rice hulls, and natural botanical binders without synthetic excipients.
Advanced dual-layer compression separating incompatible active vitamins or combining immediate-release and extended-release layers in one tablet.
Understanding the scientific rigor behind our high-speed compression lines and quality assurance protocol.
Depending on powder bulk density and flowability, we utilize direct compression for free-flowing premixes, high-shear wet granulation for dense mineral blends, or roller compaction (dry granulation) for moisture-sensitive vitamins like Vitamin C and B-complex.
Equipped with automated multi-station rotary tablet presses, our lines execute precise pre-compression and main compression stages. Hydraulic force controls maintain target tablet hardness (KP), tight weight tolerances (±1.5%), and uniform thickness.
Perforated coating pans apply uniform polymer films (HPMC, PVA, or natural cellulose derivative coats). Coating seals out ambient moisture, eliminates bitter botanical notes, prevents gastric irritation, and provides vibrant, natural color options.
During every batch run, our QC technicians perform automated physical testing every 15 minutes: checking tablet hardness, thickness, friability (<0.8%), disintegration time in simulated gastric fluid (<30 min), and individual weight variation.
Raw materials and finished tablets undergo full analytical testing at our site-licensed laboratory. HPLC assays verify active vitamin potency, while ICP-MS screens for heavy metals (lead, cadmium, arsenic, mercury) to exceed global safety standards.
Enhance brand recognition with custom-designed tablet shapes (oval, round, caplet, triangle, heart) and high-precision punches for embossed logos, product identifiers, and break-lines for adjustable dosage flexibility.
As global buyers leverage AI-driven demand analytics and navigate shifting consumer preferences, the contract manufacturing landscape for vitamin tablets is undergoing a massive transformation. B2B procurement managers and brand owners must align with manufacturers capable of delivering next-generation tablet innovations:
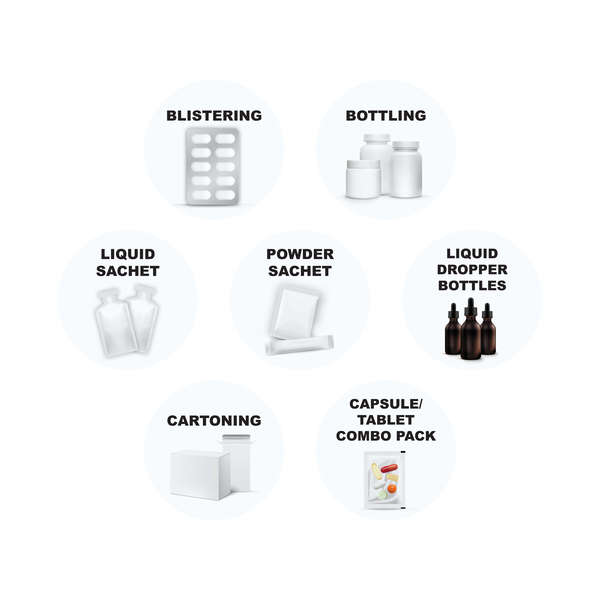
Protecting tablet stability and driving shelf appeal through controlled in-house packaging services. Bulk tablet product never leaves our GMP cleanroom until it is sealed, serialized, and boxed.
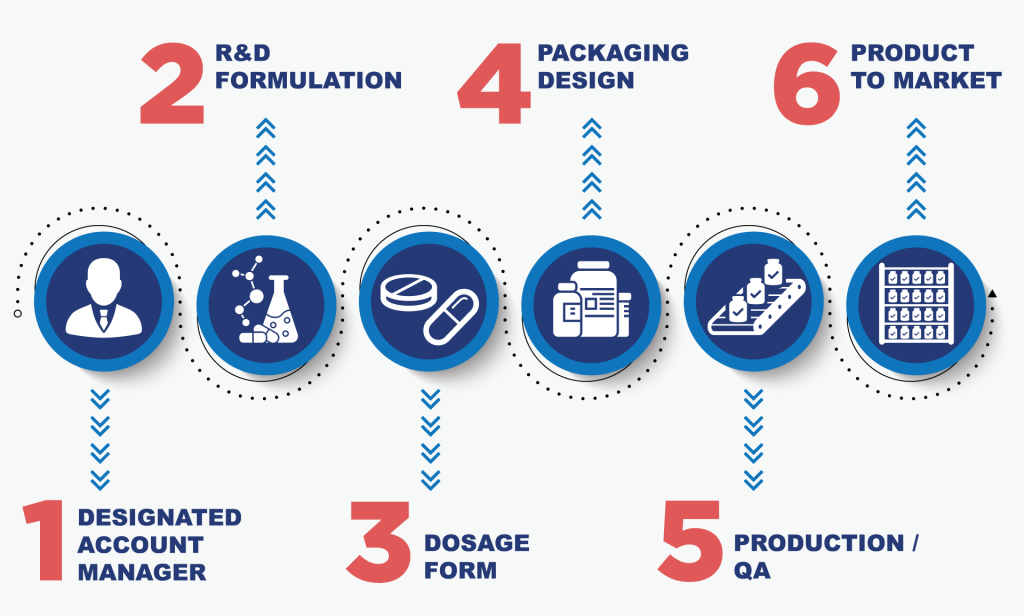
A transparent, audit-proven development path ensuring speed-to-market, regulatory security, and complete batch repeatability.
We analyze active dosages, target cost-per-tablet, dissolution criteria, and market regulations to define the exact compression method.
R&D formulators optimize granulations, evaluate excipient flow, design tablet dies/punches, and return a fixed transparent quote.
Our regulatory specialists submit Health Canada NPN applications, verify international label claims, and compile compliance dossiers.
Trial compression runs evaluate friability, hardness, disintegration, and coating adhesion before full-scale commercial manufacturing.
Commercial batch execution under automated press parameters with continuous weight and hardness monitoring and full analytical release.
In-house bottling, blister packing, or sachet filling with batch Certificates of Analysis, Free Sale Certificates, and global shipping logistics.
Global Dietary Supplement Brands Successfully Launched
Export Destination Markets Across North America, Europe & Asia
Years of Continuous Health Canada GMP Manufacturing Operations
Active Product SKUs Manufactured and Shipped Annually
International Quality Certifications & Industry Excellence Awards
Delivering total transparency, risk mitigation, and verified product quality for international supplement brands.
Our facility operates strictly under Health Canada Site License requirements and international GMP guidelines. Audited production suites ensure zero cross-contamination and complete lot traceability.
In addition to advanced tablet compression, our Scarborough plant manufactures softgels, hard capsules, liquid syrups, and powders. Consolidating your portfolio with one master supplier streamlines logistics and quality control.
Your proprietary vitamin tablet formulations remain 100% your intellectual property. We execute strict Non-Disclosure Agreements (NDAs) prior to receiving custom technical specifications.
We take the friction out of customs clearance by providing complete export documentation packages, including Certificates of Analysis (CoA), Certificates of Free Sale (CFS), and Health Canada NPN registration support.
Every account is assigned a senior technical project manager who coordinates formulation testing, regulatory submissions, packaging production, and batch shipping updates in real-time.
Whether launching a specialized niche pilot run or scaling to millions of bottles for global retail chains, our high-efficiency rotary presses scale smoothly without sacrificing quality.
"NutraLab Canada transformed our complex multi-vitamin tablet formulation from a sticky, hard-to-compress concept into a flawless, film-coated commercial product. Their regulatory team secured our Health Canada NPN in record time."
Juan NarvaezInternational Brand Manager"Finding a contract manufacturer capable of producing high-potency chewable vitamin C tablets without bitter off-notes was a major challenge. NutraLab's flavor chemists nailed the taste profile and friability."
Andrew ZhangNutraceutical Founder"Their single-source capability is unmatched. We ship tablet bottles, softgels, and powder sachets directly from NutraLab to our distributors in Europe and Asia. The export documentation is always perfect."
Gary GersonWholesale Supply Chain DirectorExpert answers to common technical, regulatory, and commercial queries asked by global procurement officers and brand founders.
Partner with Canada's premier Health Canada site-licensed contract manufacturer. Contact our technical team today to discuss formulation design, custom tooling, and competitive unit pricing.