Direct factory-grade nutritional raw materials, custom formulation capsules, and bulk dietary supplements backed by full cGMP documentation and analytical purity release standards.








The global dietary supplement and pharmaceutical capsule market has reached a critical turning point. Overseas brand owners, pharmaceutical distributors, and nutraceutical enterprises looking for premier capsule filling factories in China must evaluate partners beyond basic unit cost. True competitive advantage is forged through high-speed automation, analytical quality assurance, supply chain integration, and rigorous international certification compliance.
Modern capsule contract manufacturing relies heavily on automated tamping-pin and dosator encapsulation technology. Leading facilities operate within Class 100,000 (ISO Class 8) cleanrooms equipped with ambient temperature and humidity control system loops. This environmental isolation is vital when filling hygroscopic botanical extracts, sensitive probiotic strains, or oily bioactive formulations.
Consumer preferences and regulatory frameworks are evolving rapidly. B2B procurement managers must align with manufacturing plants capable of executing next-generation capsule technologies.
The global shift away from traditional bovine gelatin toward Hydroxypropyl Methylcellulose (HPMC) and fermented Pullulan polymers is accelerating. Non-GMO, Halal, Kosher, and Vegan certified shells are now mandatory for entering premium North American and European retail ecosystems.
Combining oil-based active liquids (such as Omega-3 fish oil or Vitamin D3) with micro-encapsulated dry beadlets or secondary targeted-release capsules in a single shell. This protects incompatible ingredients and provides sustained-release nutrient absorption profiles.
Targeted intestinal delivery without requiring synthetic film coatings. Acid-resistant HPMC capsules bypass harsh stomach gastric acids, releasing sensitive active enzymes, SAMe, or probiotic strains directly into the upper intestinal tract for maximum bioavailability.
Tier-1 manufacturing factories are integrating automated vision sorters, real-time laser weight sensors, and inline NIR spectroscopy. This catches shell defects, micro-cracks, and weight fluctuations during production runs rather than relying solely on post-batch testing.
Replacing standard softgels with hermetically nitrogen-sealed liquid hard capsules. LFHC technology eliminates plasticizers, reduces oxygen permeability, allows higher melting-point liquid formulations, and provides superior barrier defense against lipid oxidation.
Enterprise procurement teams increasingly mandate lot-level transparency from raw botanical harvest to finished capsule packaging. Modern Chinese suppliers supply QR-coded Certificate of Analysis datasets verified via immutable batch records.
Streamlining multi-SKU product portfolios through a single accredited contract manufacturer reduces audit overhead, unifies quality control benchmarks, and accelerates global market fulfillment.
Gelatin, HPMC, Enteric & Pullulan size 000 to 4.
Bioavailable lipid liquids, suspension matrices & Omega oils.
Direct compression, film-coated, chewable & effervescent.
Pediatric, geriatric & high-dose botanical syrups.
Pectin and gelatin base with precise active deposit.
Proteins, collagen peptides & pre-workout drink mixes.
A comparative strategic evaluation for brand owners deciding between contract manufacturing partnership and direct capital expenditure in manufacturing infrastructure.
| Evaluation Vector | Tier-1 OEM Contract Supplier | In-House Manufacturing Strategy |
|---|---|---|
| Capital Expenditure (CapEx) | Zero CapEx - Pay only per unit batch run | $2.5M - $8M+ for cleanroom build out & machinery |
| Regulatory Compliance Liability | Transferred - Shared auditing under supplier cGMP site licence | Full direct regulatory liability, site audits & filings |
| Production Lead Times | 3 to 6 weeks for standard stock shell re-orders | Requires internal staffing, maintenance & testing loops |
| Formulation R&D Capability | Access to dedicated in-house chemists & stability testing labs | Requires hiring internal formulation scientists |
| Analytical Quality Controls | HPLC, LC-MS/MS, ICP-MS heavy metal screening included on CoA | Substantial ongoing testing lab equipment calibration costs |
| Scaling Flexibility | Seamless scaling from pilot MOQs (50k) to multi-million runs | Constrained by fixed machine output capacity limits |
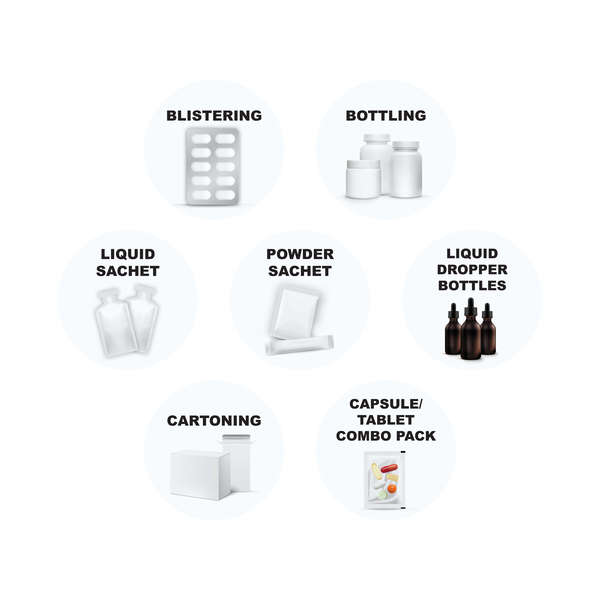
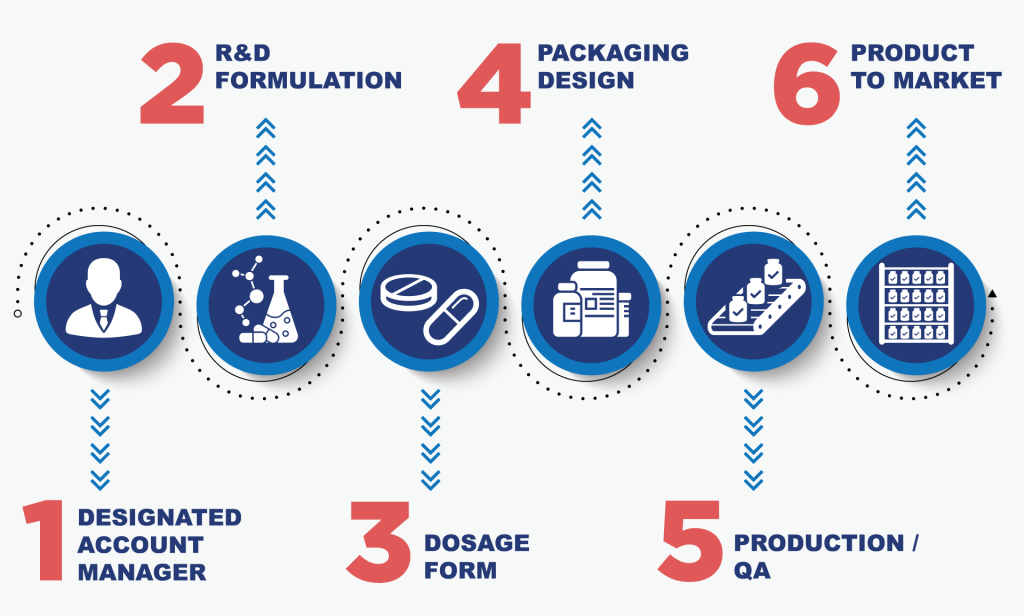
Bulk capsule filling is only half the equation. Enterprise brand owners require fully integrated, turn-key finishing services where bulk capsules never leave environmental compliance controls before final unit packaging, serialization, and containerization.
Facilities offer complete packaging capabilities tailored to target retail channels, including regional compliance checks for North America, Europe, Asia, and the Middle East:
Critical compliance, technical, and logistical answers to help supply chain managers make informed contract manufacturing decisions.
