Explore our premium bulk and private label formulations engineered for maximum bioavailability, compliance, and international retail shelf impact.








As global consumer demand shifts toward scientifically validated, clean-label, and highly bioavailable wellness products, international buyers face complex supply chain challenges. Selecting a qualified custom supplement manufacturer requires examining verifiable quality control systems, raw material traceability, and international regulatory readiness.
With over 25 years of specialized contract manufacturing expertise, our China-based state-of-the-art facility bridges the gap between raw botanical processing and finished retail goods. We operate under stringent GMP, ISO 22000, HACCP, and Halal certifications, offering end-to-end transparency for brand owners across North America, Europe, Asia-Pacific, and the Middle East.
Empowering over 500 global health brands with flexible batch sizes, scalable infrastructure, and zero-defect quality release standards.
Global Brands Successfully Brought to Market
International Export Destinations Supported
Years of Advanced OEM/ODM Manufacturing
Active SKUs Produced & Shipped Annually
Batch Quality Assurance Pass Rate
B2B importers and supplement brand strategists must align their product development with emerging scientific innovations and changing global consumer expectations.
Standard powder active ingredients often suffer from poor gastrointestinal absorption and rapid enzymatic degradation. Advanced micro-encapsulation and liposomal lipid-bilayer delivery systems protect sensitive active compounds—such as Phosphatidic Acid, TUDCA, and Shilajit fulvic acid—enhancing cellular uptake and bioavailability up to 5-fold.
Global consumers actively reject synthetic binders like magnesium stearate, silicon dioxide, and artificial colorants. Modern custom formulation engineering relies on natural organic tapioca maltodextrin, rice hull concentrated extracts, and plant-derived pectin matrixes to maintain capsule integrity without sacrificing clean-label marketing claims.
While bovine and porcine gelatin remain industry standards, vegetarian and vegan softgels utilizing carrageenan and modified starch formulations are growing rapidly. Importers targeting premium natural wellness segments are transitioning oil-based botanicals, marine peptides, and fat-soluble vitamins into 100% plant-based softgel shells.
Consolidating multi-SKU product lines under a single expert manufacturer ensures consistent quality standards, streamlined batch release protocols, and lower logistics management costs.
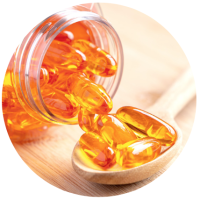
Precision encapsulation for omega-3 fish oils, CoQ10, vitamin D3/K2, and lipophilic herbal oil complexes with high dosage accuracy.
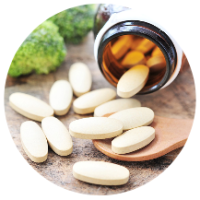
High-speed rotary tablet compression offering film-coated, chewable, effervescent, and extended-release multi-layer formulations.
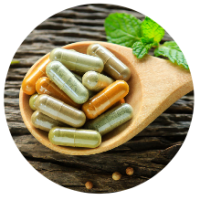
Automatic encapsulation for gelatin and HPMC vegetarian capsules filling botanical extracts, amino acids, and probiotic micro-beads.
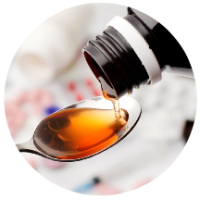
Homogeneous liquid suspensions, oral drops, and concentrated syrups engineered with advanced flavor-masking technologies.
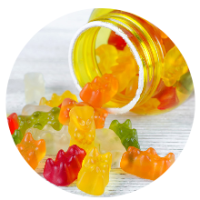
Pectin and gelatin functional gummies formulated with low sugar, natural fruit juices, and thermally stable active vitamin complexes.
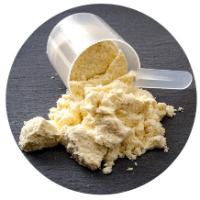
V-blender uniform mixing for sports nutrition pre-workouts, collagen powders, greens formulas, and instantized amino acids.
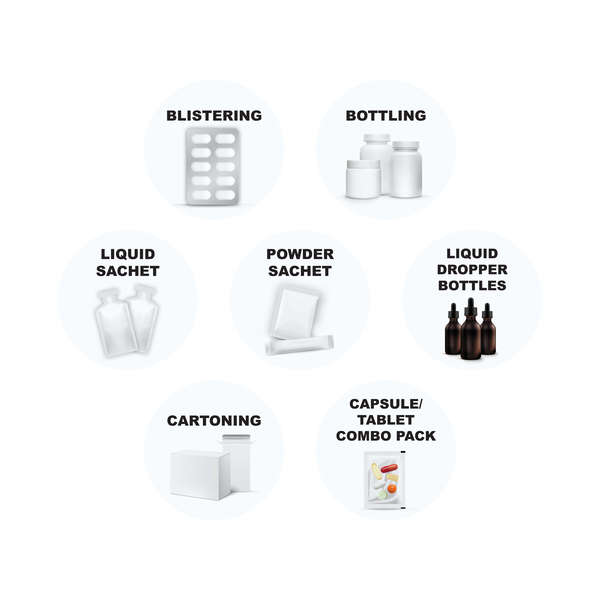
Finishing bulk products within the same controlled cleanroom facility is vital to prevent ambient moisture contamination, oxidation, and cross-exposure. Our automated packaging lines handle all secondary processing under strict batch serialization standards.
Automated tablet/capsule counting, desiccant insertion, induction sealing, and tamper-evident neck banding.
High-barrier push-through blister packaging designed for humid tropical export climates and travel portability.
Stick-packs and 4-side seal foil sachets optimized for powder beverages, marine collagen, and liquid doses.
Multi-capsule daily blister strips, custom printed outer display boxes, and shrink-wrapping for retail shelves.
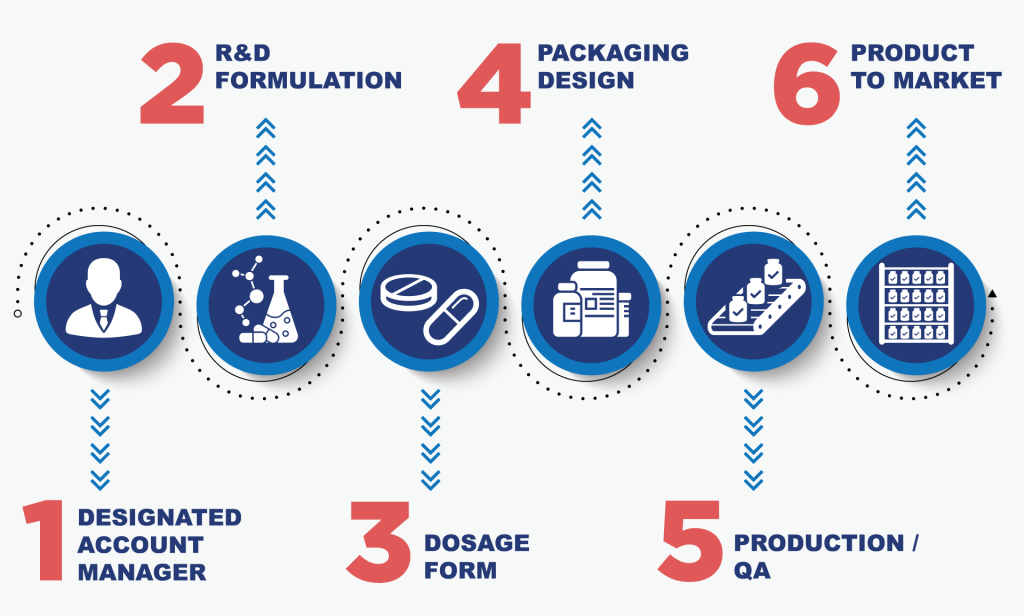
From initial formula optimization to international customs clearance, our standardized project workflow ensures total visibility, milestone control, and predictable lead times.
We analyze your target market regulations, required active dosages, label claim goals, budget targets, and projected order volumes to establish an optimized manufacturing path.
Our pharmaceutical scientists formulate raw ingredient specifications, conduct bench-scale trial blends, source qualified raw materials, and issue transparent unit cost quotes.
In-house regulatory experts review ingredient safety limits, label claims, allergen declarations, and prepare complete compliance dossiers tailored to your destination country.
We produce pilot batch samples for organoleptic and dissolution testing, while our graphic team verifies dielines, printing specs, and label compliance.
High-speed commercial batching begins in Class 100,000 cleanrooms under strict Batch Production Records (BPR), featuring in-process weight, hardness, and disintegration checks.
Finished product lots undergo micro and heavy metal testing. Upon CoA sign-off, goods are palletized, serialized, and shipped alongside complete export customs documentation.
Evaluating potential contract manufacturing partners requires rigorous technical scrutiny to avoid inventory recalls, regulatory fines, and supply disruptions.
A robust contract manufacturer must enforce strict vendor audit protocols. Every lot of active ingredient—such as Hydrolyzed Marine Collagen or Creatine Monohydrate—should undergo Fourier Transform Infrared Spectroscopy (FTIR) or High-Performance Liquid Chromatography (HPLC) to confirm chemical identity before entering production cleanrooms.
Formulations must withstand varying environmental conditions during sea freight and retail storage. Importers should confirm that manufacturers offer ICH-compliant accelerated stability testing (40°C / 75% RH) and real-time stability monitoring to validate two-to-three-year label claim expirations.
Finished dietary supplements must meet strict micro limits for E. coli, Salmonella, Staphylococcus aureus, yeast, and mold. Additionally, ICP-MS testing must verify that elemental heavy metals (Lead, Arsenic, Cadmium, Mercury) fall well below international USP and European Pharmacopoeia safety thresholds.
Whether pressing tablets or filling hard capsules, dosage weight variation must remain within tight ±2.5% control limits. Automated disintegration testing ensures that tablets and capsules break down efficiently in the digestive tract within specified timeframes (typically under 20–30 minutes).
Get instant answers regarding Minimum Order Quantities (MOQ), custom formulation IP, regulatory clearance, and international shipping protocols.
MOQs depend primarily on the dosage format and packaging selection. Powder blends (e.g., Creatine Monohydrate or Marine Collagen) typically start at 500 to 1,000 units per batch. Encapsulated capsules and compressed tablets start around 100,000 individual units or 1,000 to 2,000 finished retail bottles. Softgel encapsulation and specialized gummy production lines require larger initial batch runs (typically 300,000+ units) due to line calibration, gelatin ribbon setup, and thermal setting parameters. Contact our sales engineering team for exact tier pricing.
Standard lead time for repeat production runs is approximately 3 to 4 weeks upon raw material availability and artwork approval. First-time custom formulas generally require 6 to 8 weeks. This timeline accounts for R&D bench sample approval, raw material qualification, pilot batch assay validation, stability checks, commercial cleanroom manufacturing, finished batch laboratory testing, and CoA generation.
Yes. Our dedicated regulatory affairs department provides full documentation support to ensure your goods clear customs seamlessly in over 35 countries. We issue comprehensive export dossiers, including Certificate of Analysis (CoA) from accredited laboratories, Certificate of Free Sale (CFS), Health Certificate, BSE/TSE-Free Statements, Halal Certification, allergen declarations, and full quantitative formulation disclosures required by international border inspection agencies.
You do. Under our standard OEM contract terms, all proprietary custom formulations developed specifically for your brand remain 100% your intellectual property. We execute comprehensive Non-Disclosure Agreements (NDAs) prior to receiving technical specs or beginning formulation work, ensuring your unique ingredient combinations and trade secrets are fully protected.
Flavor consistency across bulk powder production (such as pre-workouts and BCAA mixes) is maintained through strict organoleptic reference standards and standardized V-blending procedures. We lock in approved target flavor retention profiles using micro-encapsulated natural flavors and natural spray-dried juice concentrates. Every production run is tested against baseline retain samples by our trained sensory panel before final release.
Absolutely. We specialize in clean-label manufacturing. We stock an extensive inventory of Non-GMO Project Verified ingredients, USDA Organic certified plant extracts, Kosher/Halal marine peptides, and plant-derived HPMC hard capsule shells. We can formulate your product entirely free of synthetic magnesium stearate, artificial dyes, titanium dioxide, gluten, soy, or dairy excipients.
Ready to scale your nutrition brand with pharmaceutical-grade contract manufacturing? Submit your formula specifications, desired dosage form, and volume goals to receive an optimized production plan and unit quote within 24 hours.
