Premium bulk ingredients, ready-to-label supplements, and fully custom batch configurations engineered under stringent cGMP quality protocols.








Combining over 25 years of pharmaceutical-grade manufacturing knowledge with high-capacity smart factories to support global dietary supplement brands.
An authoritative whitepaper analysis on modern nutraceutical delivery platforms, bioactive extraction, and consumer preference dynamics.
Modern consumers demand higher efficacy per milligram. Our manufacturing facilities utilize advanced liposomal encapsulation and micro-emulsification technologies to protect sensitive active compounds—such as TUDCA, CoQ10, and Glutathione—from gastric degradation. By wrapping lipophilic actives in phospholipid double-layers, cellular uptake and bio-availability increase by up to 400% compared to traditional crude powders.
Bioactive peptides are reshaping sports nutrition and anti-aging categories. Through controlled multi-stage enzymatic hydrolysis, high-molecular marine collagen proteins are cleaved into low-molecular-weight peptides (< 1,000 Daltons). This targeted enzymatic degradation guarantees complete solubility, neutral organoleptic profiles, rapid intestinal absorption, and optimized cellular signaling for joint and dermal matrix repair.
Global consumer shifts toward plant-based lifestyles have accelerated demand for gelatin-free delivery mechanisms. Our plant-derived starch and carrageenan matrix technologies allow high-temperature encapsulation of sensitive botanical oils, omega fatty acids, and lipid-bound nutrients without cross-linking risks or thermal degradation, fulfilling strict EU EFSA and US FDA clean-label criteria.
Specialized nutritional categories—such as pre-workout nitrogen pumps, mTOR pathway activators (Phosphatidic Acid 50%), and standardized adaptogens (high-fulvic acid Shilajit)—require exacting particle size distribution and micro-blending precision. High-shear multi-directional blending guarantees uniform active content per dose, eliminating hotspot variation across large industrial production lots.
Unrefined botanical extracts often present purity, heavy metal, and active marker inconsistencies. Utilizing supercritical CO2 fluid extraction and HPLC-standardized fractionation, key actives like Maca glucosinolates and Shilajit fulvic acid complexes are isolated at high concentrations while purging pesticide residues, solvent traces, and microbial contaminants.
High-purity essential amino acids such as DL-Methionine (99%) and Creatine Monohydrate require strict moisture-controlled crystallization to prevent clumping and chemical oxidation. Controlled humidity cleanrooms ensure optimal flowability, bulk density uniformity, and rapid disintegration times in finished oral dosage formats.
As a premier contract manufacturer, our operations adhere to Health Canada Site-Licensed standards, US FDA cGMP requirements, and ISO/IEC 17025 laboratory accreditation benchmarks. We provide total end-to-end transparency for global brands seeking risk-mitigated supply chains.
Every single incoming raw material undergoes strict identity testing via FTIR spectroscopy, heavy metal quantitation via ICP-MS, and microbial screening via micro-plating before entering production rooms. Full batch records are archived for complete lot traceability.
Consolidating your multi-SKU product catalog under one master supplier reduces vendor audit overhead, unifies QA metrics, and optimizes bulk freight logistics.
High bioavailability for lipophilic actives, fish oils, and botanical extracts.
Chewables, film-coated, effervescent, and time-release matrix compressed forms.
Vegetarian (HPMC) & gelatin shells for powders, botanicals, and prebiotics.
Pediatric & geriatric syrups, oral drops, and high-concentration liquid shots.
Pectin & gelatin bases with precise active dosing and natural flavoring profiles.
Protein, greens, pre-workout blends, and functional drink mixes in bulk or sachets.
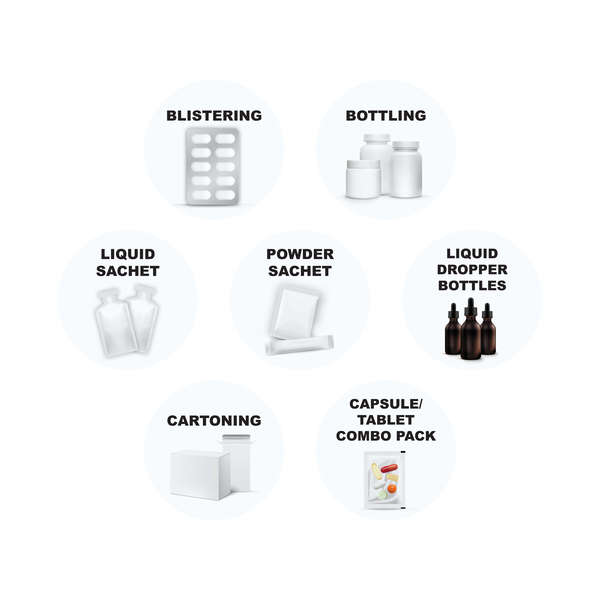
Bulk products never leave our controlled climate-regulated cleanroom environments until fully filled, induction sealed, labeled, and serialized under master batch records.
Strategic guidance for procurement executives and brand owners navigating global regulatory shifts, dual-sourcing models, and supply resilience.
Global supply chain disruptions have proven that single-source raw material procurement poses unacceptable commercial risks. Forward-thinking supplement brands require contract partners with pre-qualified dual-source supply networks for active pharmaceutical ingredients (APIs) and specialty botanicals.
Our manufacturing infrastructure integrates full blockchain-ready lot tracking from agricultural source or chemical synthesis to final packaged unit, ensuring compliance with US FSMA 204 traceability rules and European regulatory mandates.
Cross-border product expansion fails when label claims, excipients, or heavy metal limits clash with destination market regulations. Navigating maximum daily intake limits for ingredients such as TUDCA, Marine Collagen, or Phosphatidic Acid demands deep regulatory oversight.
We offer complete regulatory dossier support—including Health Canada NPN applications, US FDA structure/function claim reviews, and Certificate of Free Sale (CFS) generation—enabling seamless market entry across 35+ countries.
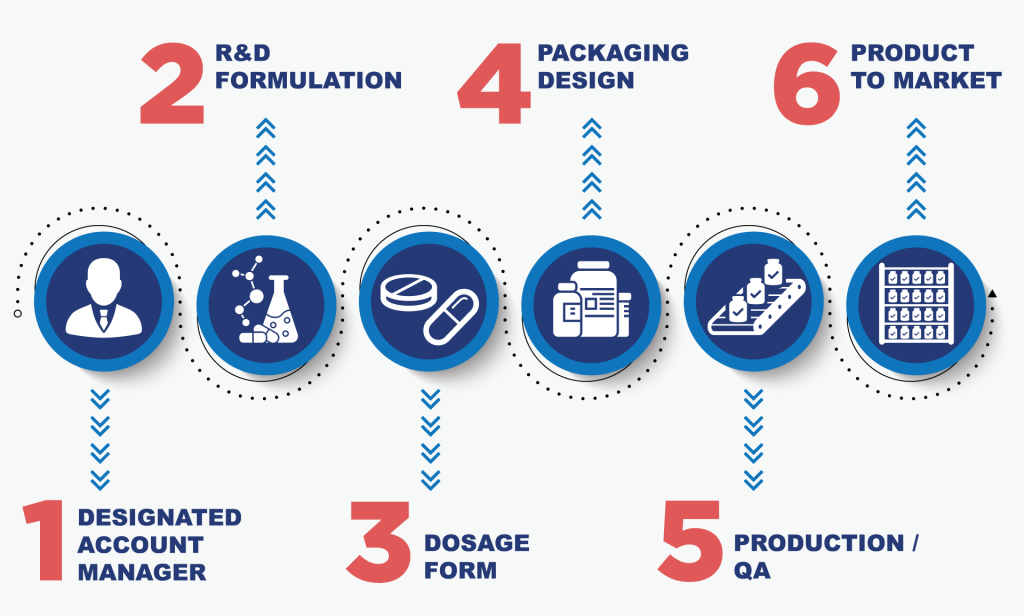
From initial formulation consultation to final international export shipping, every stage is governed by clear timelines and rigorous QC checkpoints.
We evaluate your target market, budget, dosage format preferences, and regulatory constraints to establish technical manufacturing specifications.
Our R&D laboratory formulates pilot samples, verifies active stability, and returns a detailed commercial quotation with clear MOQ tiers.
In-house regulatory specialists audit label compliance, review artwork specifications, and submit necessary dossiers to regulatory authorities.
Bench-scale pilot batches undergo accelerated stability, organoleptic validation, and dissolution testing prior to full industrial scale-up.
Bulk production proceeds in certified cleanrooms. Finished products are held until our QA lab issues a signed Certificate of Analysis (CoA).
Bottling, blistering, and cartoning are finalized in-house. Freight documentation, customs documentation, and certificates are serialized for export.
Direct technical answers addressing minimum order quantities, regulatory filings, quality assurance protocols, and private label timelines.
Elevate your supplement brand with cGMP-certified manufacturing, advanced bio-availability research, transparent pricing, and rapid global delivery.
Get a Quote