Standardized formulations ready for rapid custom packaging, white-label branding, and compliant global export.



The global dietary supplement market is undergoing a structural paradigm shift driven by heightened consumer scrutinization of raw material sourcing, bio-efficacy, and transparent analytical validation. For international nutraceutical brands, pharmaceutical chains, and digital-first health enterprises, navigating the landscape of China Wholesale OEM Supplements Manufacturers & Suppliers requires moving beyond basic cost-per-unit metrics to evaluating long-term technical competence, supply chain agility, and international regulatory compliance.
China has established itself as the world's primary epicenter for active pharmaceutical ingredients (APIs), standardized botanical extracts, amino acid bio-fermentation, and high-capacity nutraceutical dosage form manufacturing. However, leading global brands recognize that true supply chain resilience depends on selecting an OEM partner that bridges high-volume raw material dominance with rigorous Western regulatory frameworks such as cGMP, Health Canada Site Licensing, ISO 22000, and US FDA registration standards.
By leveraging advanced microencapsulation, liposomal delivery technologies, and fully integrated in-house packaging lines, modern contract manufacturers ensure that every bulk production run meets stringent limits for purity, heavy metals, microbial safety, and active potency stability throughout shelf life.
Consolidating multi-format SKU portfolios under one certified contract manufacturer eliminates vendor fragmentation, standardizes quality assurance protocols, and significantly accelerates landed lead times.
Specialized rotary die encapsulation for lipid-soluble bio-actives including ultra-pure fish oil (EPA/DHA), CoQ10, Vitamin D3/K2, Astaxanthin, and herbal oil extractions. Available in animal gelatin or plant-based Tapioca/Carrageenan vegan shells with customizable color, shape, and enteric coating option for optimal gastric bypass.
High-speed rotary press technology producing direct-compression, chewable, sublingual, effervescent, and multi-layer sustained-release tablets. We maintain precise friability and hardness controls alongside aqueous film or enteric coatings to protect sensitive botanical actives against oxidation.
Automated capsule filling lines capable of handling dry powders, micro-pellets, and liquid-fill combinations. Options include pharmaceutical gelatin, HPMC vegetable capsules, and pullulan shells without synthetic excipients, binders, or artificial flowing agents.
Formulation of oral liquids, herbal syrups, drops, and functional tonics with engineered particle suspension and organoleptic flavor masking. Produced under sterile liquid fill conditions with precise pH stabilization and thermal pasteurization.
Advanced starchless depositing technology producing low-sugar or sugar-free functional gummies enriched with vitamins, minerals, botanical extracts, and probiotics. Formulated with natural fruit juice pectin for clean-label market positioning.
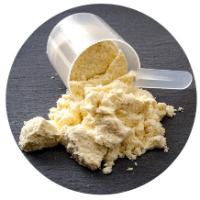
V-blender and ribbon mixer processing for sports nutrition, protein matrices, collagen peptide blends, pre-workout matrix powders, and meal replacements. Complete homogeneity testing guarantees ingredient distribution accuracy across bulk batches.
A continuous quality record requires that bulk manufactured products remain within a strictly controlled environment until sealed inside their final delivery packaging. Uncertified transport of bulk softgels or tablets to secondary packaging facilities introduces contamination risks, humidity exposure, and potential batch record gaps.
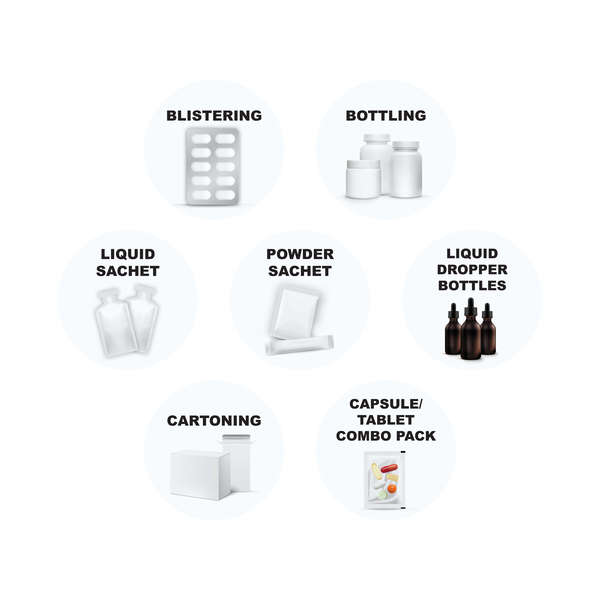
Our facility houses high-speed, automated secondary packaging suites configured for diverse commercial channels—from retail bottles to clinical blisters and single-serve e-commerce stick packs.
Staying competitive in the rapidly evolving dietary supplement landscape requires brand owners and sourcing managers to align with next-generation formulation trends, manufacturing innovations, and regulatory shifts.
Shift from traditional chemical extraction to sustainable precision fermentation. Key ingredients like Phosphatidic Acid, TUDCA, and high-purity amino acids are increasingly synthesized via bio-fermentation to guarantee non-GMO purity, zero pesticide residues, and carbon-neutral production footprints.
Global regulatory bodies and health-conscious consumers are rejecting magnesium stearate, silicon dioxide, and synthetic titanium dioxide. Modern OEM lines utilize organic rice hull concentrates, tapioca maltodextrin, and natural bamboo silica as inert flowing agents.
Nutraceutical bioavailability is paramount. Demand is surging for liposomal encapsulation, micro-emulsified lipid carriers (SMEDDS), and targeted enteric release mechanisms that protect fragile bioactive peptides (such as Marine Collagen and Glutathione) from gastric breakdown.
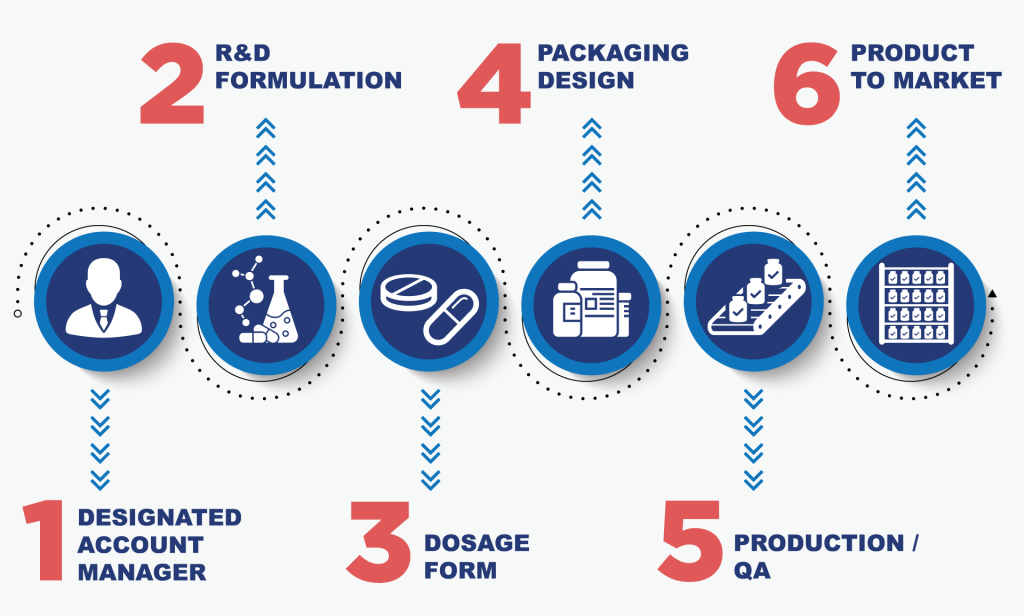
Our structured project management protocol guarantees transparent milestone reporting from initial technical feasibility review to global logistics dispatch.
Evaluation of raw material parameters, dosage form selection, target market regulatory constraints, unit target costs, and volume expectations.
Lab pilot batch formulation, active ingredient assay testing, excipient optimization, and formal price quote issuance.
Health Canada NPN registration support, label compliance review, Certificate of Analysis specification setup, and customs documentation prep.
Finalization of mechanical artwork, die-line verification, packaging mock-ups, and customer physical sample sign-off.
Automated raw material dispensing, blending, encapsulation/compression, in-process weight uniformity testing, and analytical release.
Primary bottling or blistering, secondary cartoning, palletizing under climate control, Certificate of Free Sale issuance, and freight dispatch.
Detailed evaluation framework to assist international B2B buyers in verifying enterprise credibility, technical compliance, and product quality assurance.
| Evaluation Parameter | Certified Tier-1 OEM Manufacturer | Unaccredited Trading Middlemen |
|---|---|---|
| Quality Certification | ✓ Health Canada Site License, cGMP, ISO 22000, Halal certified facilities | ❌ Third-party outsourced certificates; no direct site liability |
| Traceability & Testing | ✓ Full raw material identity testing (FTIR/HPLC), micro limits & heavy metal CoAs per lot | ❌ Generic CoAs without raw batch validation or internal laboratory testing |
| Intellectual Property | ✓ NDA-enforced custom formulation protection; customer owns formula IP | ❌ Formulas often shared across competing unbranded sellers |
| In-House Packaging | ✓ Complete secondary bottling, blister, sachet, and cartoning lines | ❌ Bulk product shipped to secondary unverified packaging sites |
| Regulatory Support | ✓ Direct support for NPN submissions, Free Sale Certificates & Export documentation | ❌ Limited or zero international regulatory compliance assistance |
| Batch Consistency | ✓ Validated blending procedures and strict in-process weight/dissolution controls | ❌ High variable rate in active content and tablet friability between batches |
Expert guidance on minimum order quantities, lead times, regulatory compliance, and formulation capabilities.