Explore our turnkey bulk supplies and private label solutions manufactured under rigorous analytical quality control, complete traceability, and international regulatory compliance.








A comprehensive analysis of technical extraction methodologies, regulatory compliance metrics, and market intelligence for global nutraceutical brand architects.
The global botanical extracts and dietary supplement manufacturing industry is undergoing a paradigm shift driven by consumer demand for clean-label, standardized bioactive ingredients and stringent international regulatory frameworks. Modern brand owners no longer evaluate contract manufacturers solely on unit price per bottle; instead, technical capability, bio-assay standardization, heavy metal screening, solvent residue control, and verified regulatory traceability dictate market success.
As a Health Canada site-licensed and cGMP-compliant contract manufacturer operating from Scarborough, Ontario, NutraLab Canada Corp. brings over 25 years of specialized expertise to the contract manufacturing landscape. Our facility integrates state-of-the-art phytochemical extraction technology, custom formulation engineering, and full-spectrum in-house dosage execution—spanning softgels, compressed tablets, two-piece hard gelatin and vegetarian capsules, functional powders, chewable units, and liquid syrups.
Achieving physiological efficacy requires precise preservation of volatile terpene profiles, polyphenolic bioflavonoids, alkaloids, and glycosides without thermal degradation or toxic organic solvent contamination. The choice of extraction technology directly influences bio-availability, batch-to-batch repeatability, and finished goods stability.
| Extraction Methodology | Target Actives & Compounds | Solvent Residue & Purity Profile | Bio-Availability Index | Primary Application Formats |
|---|---|---|---|---|
| Supercritical CO2 Extraction | Lipids, Essential Oils, Phytocannabinoids, Astaxanthin | Zero Organic Solvents (Non-toxic CO2 loop) | Exceptionally High (95-99%) | Softgels, Liquid Droppers, Liposomal Suspensions |
| Hydro-Ethanolic Extraction | Polyphenols, Flavonoids, Glycosides, Maca Extract | Strict USP/EP Residual Solvent Limits (<50ppm) | High (85-92%) | Two-Piece Capsules, Chewable Tablets |
| Enzymatic Hydrolysis | Collagen Peptides, Hydrolyzed Proteins, Marine Bioactives | Zero Toxic Byproducts, Controlled Daltons | Ultra-High (Low Mol. Weight) | Soluble Powders, Functional Beverages |
| Membrane Ultrafiltration | Soy Phosphatidic Acid, Phospholipids, Amino Acids | Solvent-Free Aqueous Separation | High Bio-affinity | Pre-Workout Blends, Nootropic Capsules |
By employing standardized high-performance liquid chromatography (HPLC), gas chromatography-mass spectrometry (GC-MS), and inductively coupled plasma mass spectrometry (ICP-MS) testing protocols, we guarantee that every batch of botanical extract yields measurable marker compound concentrations while strictly adhering to international limits for lead, arsenic, cadmium, mercury, pesticides, and microbial pathogens.
Key market vectors shaping supply chain decisions, consumer buying behaviors, and formulation engineering through 2030.
Global buyers are abandoning raw plant powders in favor of standardized extracts with verified active assays (e.g., 50% Phosphatidic Acid from Soy, 60% Fulvic Acid in Shilajit). Brand trust relies on batch-to-batch chemical equivalence verified via HPLC chromatograms.
Adulteration in the botanical supply chain has elevated the need for genomic authentication. Regulatory bodies mandate DNA barcoding to confirm that raw botanicals are species-pure without synthetic spiking or unlabelled species substitution.
High dose concentrations are ineffective without gut mucosa permeability. Future trends heavily favor micro-encapsulation, liposomal delivery, and hydrolyzed peptides (such as Marine Collagen Peptides) that bypass enzymatic degradation for systemic cellular absorption.
Single-ingredient SKUs are giving way to complex, target-specific formulations. Blending adaptogenic botanicals like Maca and Shilajit with hepatic compounds like TUDCA or metabolic amino acids like DL-Methionine creates proprietary IP that drives customer retention.
Integrating 25 years of Canadian manufacturing pedigree with global export support, full regulatory licensing, and single-site operational efficiency.
NutraLab Canada operates a modern, Health Canada site-licensed facility at 980 Tapscott Rd, Scarborough, Ontario. Our site is engineered under strict cGMP protocols, equipped with temperature- and humidity-controlled cleanrooms, air filtration handling systems, and automated production machinery.
Choosing a Canadian manufacturer grants international buyers an immediate competitive advantage: Canada’s regulatory environment for Natural Health Products (NHPs) is among the most stringent worldwide. Products manufactured in our facility receive international credibility, smooth customs clearance, and audit-ready documentation packages.
Optimal for lipophilic botanical oils, marine fish oils, CoQ10, and fat-soluble vitamin suspensions with zero leakage.
Chewable, coated, sublingual, and extended-release formats engineered for precise weight uniformity and hardness.
Gelatin, HPMC vegetarian, and delayed-release acid-resistant capsules tailored for botanical powders and probiotics.
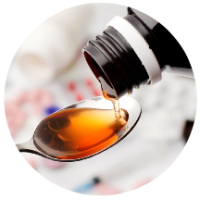
High-solubility botanical elixirs, pediatric syrups, and concentrated tinctures featuring custom flavor masking.
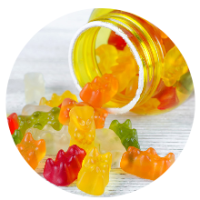
Pectin-based vegan and gelatin nutraceutical gummies crafted with natural botanical colors and delicious fruit flavors.
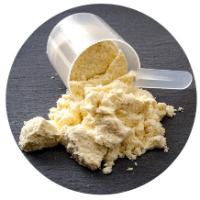
Homogeneous high-volume powder blending for sports nutrition, greens, hydrolyzed collagen, and functional stick-packs.
Bulk product never leaves our controlled environmental cleanrooms unsealed. By retaining packaging in-house, we eliminate external transport risks, prevent cross-contamination, and streamline lot serialization.
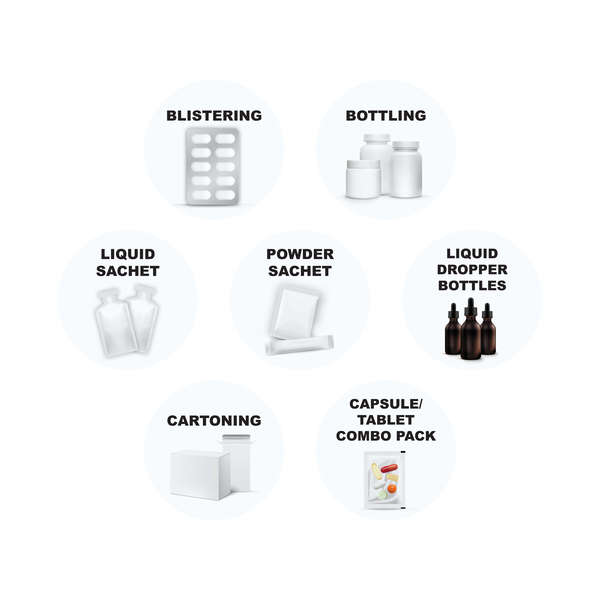
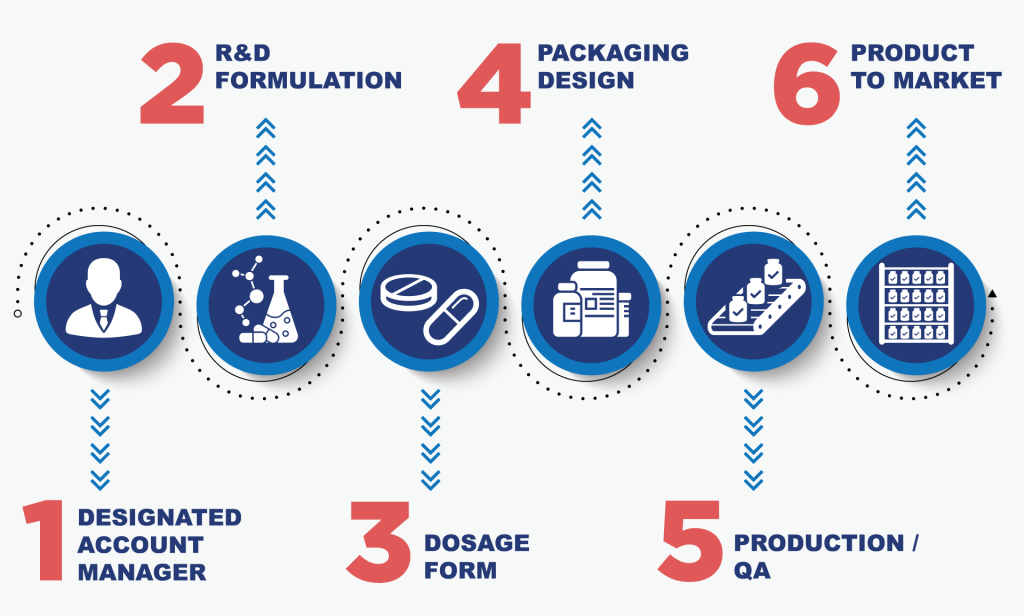
A structured, audit-tracked workflow designed to transform custom formulation concepts into commercial market-ready products.
We review your target market claims, dosage preference, annual volume expectations, and regulatory destination requirements.
Our master formulators select standardized ingredients, evaluate physical stability, and supply a transparent cost breakdown.
In-house regulatory scientists verify label claim compliance and submit Natural Product Number (NPN) applications to Health Canada.
We run pilot samples for physical inspection and verify artwork dielines, barcode placement, and label compliance checks.
Commercial production executes under master batch records with in-process weight, hardness, micro, and assay checks.
Finished goods are issued a signed Certificate of Analysis (CoA) and packed with export customs documentation for immediate dispatch.
Expert answers addressing minimum order quantities, regulatory licensing, lead times, and custom formulation parameters.
Minimum order quantities depend directly on the chosen dosage form and packaging format. Solid dosage formats such as tablets and two-piece capsules typically start at lower minimum runs (often 100,000 units), whereas softgel encapsulation and gummy production lines require larger batch volumes (typically 300,000+ units) to maintain active ingredient homogeneity, mass variation tolerances, and machine calibration stability. Each written quotation outlines exact MOQ tiers and unit pricing scales.
A standard custom manufacturing cycle spans 6 to 10 weeks following final artwork approval and raw material analytical qualification. Stock formulations with pre-existing raw material inventory move significantly faster (3 to 4 weeks). If your product requires a new Health Canada Natural Product Number (NPN) licensing submission, regulatory review times will add an additional window prior to commercial release.
Yes. Our in-house regulatory affairs department manages the entire Natural Product Number (NPN) application workflow, including safety data dossiers, master file preparation, and health claim justifications. Furthermore, for international clients exporting to over 35 countries, we issue full Certificate of Analysis (CoA), Certificate of Free Sale (CFS), cGMP Compliance Certificates, and sanitized batch records tailored for local customs authorities.
Every raw material shipment undergoes mandatory quarantine upon arrival at our Scarborough facility. Our Quality Control laboratory executes testing using High-Performance Liquid Chromatography (HPLC) for chemical assay identification, Inductively Coupled Plasma Mass Spectrometry (ICP-MS) for heavy metal limits (Lead, Mercury, Cadmium, Arsenic), and USP micro-screening for E. coli, Salmonella, yeast, and mold before raw materials are released to production.
Your brand retains 100% intellectual property ownership of all custom formulations, proprietary ingredient ratios, trade dress, and packaging artwork developed during your project. Non-Disclosure Agreements (NDAs) are executed prior to formulation sharing to safeguard your brand’s commercial secrets.
Partner with Canada's premier Health Canada site-licensed contract manufacturer. Submit your project requirements today for immediate dosage engineering guidance, analytical cost breakdowns, and lead-time scheduling.
Get a Quote