Explore our core portfolio of validated contract blending formulations, engineered under strict pharmaceutical GMP standards for maximum bioavailability, stability, and consumer compliance.








With 25 years of pharmaceutical-grade experience at our Health Canada site-licensed facility in Scarborough, Ontario, we mitigate supply chain risk, ensure absolute formula homogeneity, and accelerate time-to-market.
Our operation is strictly governed under Health Canada Site License parameters and current Good Manufacturing Practices (cGMP). Every batch undergoes rigid raw material verification, micro-screening, heavy-metal ICP-MS analysis, and strict batch-record archival to guarantee complete audit readiness.
Navigating cross-border compliance demands expert oversight. Our specialized in-house regulatory desk manages Natural Product Number (NPN) applications, label compliance validation, Certificate of Analysis (CoA) generation, and Certificate of Free Sale (CFS) issuing across 35+ international markets.
Formulating active nutritional blends requires micro-particle dispersion without localized hotspots. Utilizing pharmaceutical-grade Ribbon, V-Blenders, and High-Shear Granulators, we ensure micro-ingredients (vitamins, trace minerals, enzymes) achieve absolute content uniformity across metric-ton output batches.
Consolidate your supply chain under one roof. From raw active ingredient procurement, custom flavor system engineering, and powder/liquid blending to final dosage encapsulation and packaging finishing—eliminating multi-vendor fragmentation and reducing total lead times.
Your custom formulation assets represent vital market equity. We operate under stringent non-disclosure agreements (NDAs) and custom contract terms, preserving 100% intellectual property (IP) ownership for brand owners, clinical research entities, and distribution partners.
Bulk product never leaves controlled ambient zones prior to sealing. Our Scarborough facility features fully automated high-speed bottling, blister thermoforming, stick-pack liquid sachets, powder pouching, and automated serialization lines designed for zero cross-contamination.
Whether your target demographic demands rapid-dissolve powders, liposomal liquids, or pharmaceutical-grade capsules, our facility delivers end-to-end manufacturing flexibility.
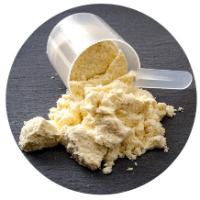
Homogeneous dry blends, instantized sports mixes, & greens formulations.
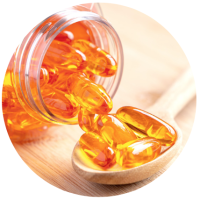
High-bioavailability lipid carriers, marine oils, & CoQ10 matrixes.
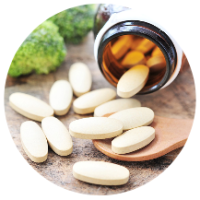
Coated, chewable, sustained-release, & multi-layer compression.
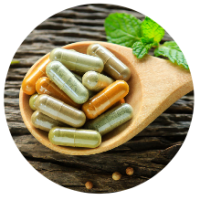
HPMC vegetarian & gelatin shells for botanicals & synthetics.
Flavor-masked syrups, botanical tinctures, & liquid suspension blends.
Pectin-based & gelatin functional gummies with precise active dosing.
An operational overview for brand managers, formulators, and corporate procurement directors regarding industrial-scale nutraceutical powder and liquid homogenization.
Industrial OEM/ODM contract blending is fundamentally a balance of particle mechanics, fluidization science, and shear forces. In nutraceutical manufacturing, a single batch may incorporate over 30 distinct raw materials—ranging from fine botanical extracts with hydroscopic characteristics to dense crystalline amino acids like Creatine Monohydrate and hydrophobic lipid peptides.
Achieving a high degree of homogeneity (low Coefficient of Variation, CV < 5%) requires selecting the correct mechanical blending profile:
Understanding the structural differences between OEM (Original Equipment Manufacturing) and ODM (Original Design Manufacturing) dictates how formulation IP, regulatory filing schedules, and raw material supply networks interact during contract operations.
| Operational Parameter | OEM Contract Manufacturing | ODM Custom Formulation Services | White-Label Stock Formulations |
|---|---|---|---|
| Formulation Ownership | 100% Brand Client Owned | Joint / Proprietary Custom IP Transfer | Manufacturer Owned & Licensed |
| R&D Lead Time | Rapid (Client Specs Provided) | 4–8 Weeks (Formulation & Pilot Runs) | Immediate (Pre-Validated Shelf Formulations) |
| Health Canada NPN Status | Client or Manufacturer Assisted Filing | Custom Master File Submission | Pre-Licensed Active NPN Available |
| Flavor & Organoleptic Masking | Executed to Client Specification | Custom Engineering & Stability Testing | Standardized Market Flavors |
| Ideal Target Customer | Established Enterprise Brands & Pharmacies | Innovative Clinical & Functional Brands | E-Commerce Startups & Fast Retail Launch |
Modern contract blending facilities operating in tier-one jurisdictions must enforce strict allergen control programs. Ingredients such as soy-derived Phosphatidic Acid, milk-derived whey isolates, fish-derived hydrolyzed marine collagen, and non-allergenic botanical powders share processing space under stringent HVAC zoning.
Our Scarborough plant enforces ISO Class 8 equivalent air-handling systems with positive-pressure HEPA filtration, automated Clean-In-Place (CIP) / Dry-Clean protocols, and validated analytical swab tests (ELISA & ATP testing) between production batches to prevent cross-contact at sub-ppm levels.
Strategic market analysis detailing consumer shift dynamics, ingredient technology advancements, and global regulatory changes shaping contract purchasing strategies.
Global distributors are actively phasing out traditional synthetic flow agents, silicon dioxide, and magnesium stearate in favor of natural rice hull extracts, organic acacia fiber, and sunflower lecithin binders. Contract manufacturers with advanced micro-blending capabilities can achieve precise powder flowability without sacrificing clean-label marketing claims.
Consumer demand for high-potency ingredients like Shilajit Extract, TUDCA, and Marine Collagen Peptides is driving the adoption of microencapsulated powder matrices. Liposomal powder blending protects active phytonutrients and biliary acids from gastrointestinal degradation, improving bio-absorption profiles by up to 400% over standard crude extracts.
Global buyers are placing stringent audit requirements on raw ingredient provenance. Ingredients like Halal-certified marine collagen peptides and pure synthetic-free DL-Methionine require complete ocean-to-bottle traceability, heavy metal verification, and eco-sustainable harvesting documentation to pass regulatory customs checkpoints.
While traditional HDPE and PET bottles remain industry staples, procurement trends show a rapid multi-year growth trajectory toward single-serve liquid sachets, stick-pack powder pouches, and 100% PCR (Post-Consumer Recycled) packaging formats that reduce shipping footprint and align with corporate ESG guidelines.
Clear, direct answers regarding minimum order quantities, manufacturing timelines, quality testing, and regulatory licensing support.
Minimum Order Quantities depend on the dosage delivery system and packaging selection. For custom dry powder blending (such as Pre-Workout formulas or Collagen powders), MOQs typically start at 1,000 units for standardized packaging formats or 500 kg for bulk powder drums. Encapsulated products (such as TUDCA or Shilajit capsules) generally start at 100,000 capsules per production run. Exact tier pricing and batch volume quotes are provided following initial technical consultation.
A turnkey contract manufacturing project follows a structured 6-phase timeline: 1) Initial Consultation & Spec Review (1 week), 2) R&D Formulation & Flavor Optimization (2–3 weeks), 3) Regulatory Licensing & Label Review (2–4 weeks), 4) Raw Material Procurement & In-House Testing (2–3 weeks), 5) Commercial Blending & Packaging Execution (2 weeks), and 6) Quality Release & Export Shipping (1 week). Repeat re-orders move significantly faster, typically shipping within 3 to 4 weeks of order confirmation.
Yes. Our experienced in-house regulatory affairs team manages full Health Canada Natural Product Number (NPN) dossier submissions, label claim reviews for FDA/Health Canada compliance, and complete export documentation packages—including Certificates of Analysis (CoA), Certificates of Free Sale (CFS), and Good Manufacturing Practice (GMP) compliance statements accepted across 35+ countries.
Every raw ingredient undergoes quarantine and identity testing (FTIR / HPLC) prior to batch release. Post-blending, finished goods undergo rigorous analytical verification, including active ingredient potency assaying, heavy metal screening (Lead, Arsenic, Cadmium, Mercury via ICP-MS), microbial limit testing (Total Aerobic Count, Yeast & Mold, E. coli, Salmonella), and physical dispersion/solubility analysis. Finished goods are released only when accompanied by a signed Certificate of Analysis.
Your brand retains 100% ownership of your proprietary formulations, custom flavor matrices, and brand graphics. All technical discussions and technical specifications are protected under binding Non-Disclosure Agreements (NDAs) executed prior to formula development.
Packaging finishing is conducted 100% in-house at our Scarborough, Ontario manufacturing plant. We offer high-speed bottling with induction sealing, blister thermoforming, liquid sachet filling, powder pouching, and capsule/tablet combination pack filling. Maintaining blending and packaging under one site license ensures unbroken chain-of-custody and complete traceability under a single Master Batch Record.
Partner with a Health Canada Site-Licensed, cGMP-certified Canadian manufacturer with 25 years of operational excellence. Contact our technical team today to receive formula feedback, batch pricing tiers, and realistic launch timelines.
Inquire Now