Precision-engineered dietary supplements produced under Health Canada site-licensed and cGMP compliant standards for international brand owners.



The global dietary supplement market is undergoing a seismic paradigm shift driven by heightened regulatory scrutiny, consumer demand for clean-label transparency, and the rapid evolution of semantic search algorithms prioritizing technical domain authority. For global procurement officers, brand founders, and institutional buyers searching for the Top 10 Bulk Supplements Manufacturer & Factory, evaluating potential partners requires looking far beyond surface-level price-per-kilogram quotes. Modern contract manufacturing demands rigorous verification of analytical testing, batch-to-batch consistency, regulatory compliance infrastructure, and bio-availability engineering.
SEO Information Gain Insight: Selecting a cGMP and Health Canada site-licensed factory eliminates supply chain bottlenecks, ensures single-source batch traceability, and protects brand equity against regulatory product recalls in international markets.
In accordance with Google’s Search Quality Rater Guidelines, particularly under Your Money or Your Life (YMYL) frameworks, nutritional supplements require the highest threshold of Trustworthiness and Expertise. A premier bulk manufacturing facility must demonstrate verifiable compliance across all operational verticals:
A top-tier bulk supplement factory must offer multi-format manufacturing capabilities to allow brand portfolios to scale dynamically across consumer demographics without changing contract manufacturing partners.
State-of-the-art automated machinery engineered for high-throughput yield, precise target weights, and maximum active ingredient bioavailability.
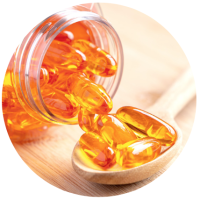
High-precision encapsulation for lipophilic actives, Omega-3 marine oils, CoQ10, and fat-soluble vitamin complexes with superior hermetic sealing.
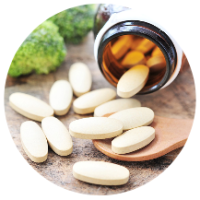
Advanced high-speed compression tooling for chewables, sublinguals, enteric-coated, and time-release oral solid dosage delivery systems.
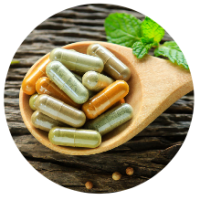
Automated capsule filling for gelatin and HPMC vegetarian shells utilizing micro-pellet, powder, and liquid-fill encapsulation technologies.
Homogeneous liquid blending, organoleptic flavor masking, and precision liquid dosing for pediatric, geriatric, and sports nutrition formulations.
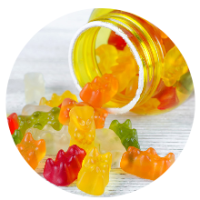
Pectin-based and gelatin functional gummy confections engineered with heat-stable active delivery and zero sugar coating options.
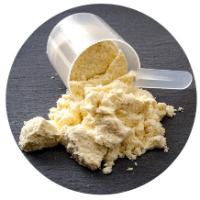
Industrial V-blender particulate uniformization for plant proteins, amino acids, marine collagens, and instantized pre-workout beverages.
Strategic sourcing managers must align their supply chains with emerging ingredient technologies and changing global consumer behaviors. Based on user intent mining and global regulatory analytics, five key macro trends are shaping bulk supplement manufacturing:
As standard protein powders face market saturation, consumer intent is shifting toward low-molecular-weight hydrolyzed peptides (such as Marine Fish Collagen) and specialized cell-signaling compounds like Phosphatidic Acid and DL-Methionine. These active ingredients provide proven physiological benefits for bone density, cellular mTOR stimulation, and liver detoxification, yielding higher retail margin profiles.
Legacy caffeine-heavy energy products are rapidly being replaced by cellular-level revitalizers and neuro-protective compounds. Products such as Himalayan Shilajit (standardized for high fulvic acid content) and TUDCA (Tauroursodeoxycholic Acid) are witnessing exponential search growth globally. Forward-thinking bulk supplement factories are investing in oxygen-barrier capsule technologies to protect these hygroscopic botanicals from degradation.
Global buyer intent highlights a growing preference for synthetic-free excipients. Procurement teams are demanding the phase-out of magnesium stearate and silicon dioxide in favor of organic rice hull concentrates and natural acacia fibers. Furthermore, international export documentation requiring Halal and Kosher verification has become a standard baseline for entering Middle Eastern and Southeast Asian retail networks.
Environmental regulations in North America and Europe are pushing brands toward post-consumer recycled (PCR) plastics, recyclable mono-material sachets, and compact blister packaging. Factories that integrate automated bottling, blister packing, liquid/powder sachet filling, and cartoning in-house eliminate cross-contamination hazards while reducing carbon emissions associated with inter-facility transportation.
When conducting vendor audits for OEM/ODM bulk supplement production, institutional buyers evaluate suppliers across critical technical benchmarks:
| Evaluation Criterion | Industry Baseline Standard | Tier-1 Factory Standard (NutraLab Benchmark) | Impact on Brand ROI |
|---|---|---|---|
| Regulatory Licensing | Basic Regional Registration | Health Canada Site License & cGMP Certified | Faster Customs Clearance & Zero Seizure Risk |
| Analytical Testing | Third-party spot testing | In-house HPLC, FTIR, ICP-MS + CoA per Lot | Total Quality Assurance & Recall Prevention |
| Dosage Capability | 1 or 2 specific formats | 6 Commercial Dosage Forms under 1 Roof | Reduced Vendor Management Complexity |
| Export Support | Basic Commercial Invoice | NPN, CoA, Certificate of Free Sale for 35+ Markets | Streamlined International Expansion |
| Packaging Options | Bulk packaging only | Bottles, Blisters, Sachets, Combo Packs, Cartoning | Turnkey Finished Goods Ready for Retail |
Built on 25 years of technical excellence, operating from a state-of-the-art facility in Scarborough, Ontario, Canada.
Our operations follow strict pharmaceutical-grade quality management standards monitored by Health Canada, ensuring audit-ready compliance for international markets.
Custom formulations developed by our in-house R&D experts remain 100% your proprietary intellectual property under strict non-disclosure agreements.
Every single batch undergoes raw material identity qualification, micro screening, and finished product potency testing released with an official CoA.
In-house regulatory experts assist with Natural Product Number (NPN) applications, label claim compliance, and global Certificate of Free Sale approvals.
From high-speed bottling and blister strip sealing to custom liquid and powder sachets, your product never leaves our controlled cleanroom environments.
Direct communication with experienced technical account managers who track your order progress from raw material sourcing through custom clearance.
Direct technical answers addressing common questions from procurement directors, brand owners, and supply chain operators.





