Direct bulk supply and contract manufacturing solutions with Health Canada site licensing, strict GMP compliance, and full international export documentation packages.

Premium bioactive type I marine collagen derived from wild-caught deep-sea fish. Optimized molecular weight (<2000 Da) ensures max bio-absorption for joint, bone, and skin health.
Contact Us
Advanced nitrogen pump formula combining L-Arginine, Beta-Alanine, and Nitric Oxide boosters. Designed for cellular stamina, vasodilation, and lean muscle mass recovery.
Contact Us
Patented mTOR activator standardized to 50% active Phosphatidic Acid. Ideal for high-potency muscle protein synthesis supplements and functional beverage fortification.
Contact Us
Ultra-micronized 200-mesh Creatine Monohydrate for maximum solubility and cell hydration. Zero fillers, unflavored, third-party lab tested for purity and heavy metal control.
Contact Us
Synergistic herbal formula combining concentrated Peruvian Black Maca root extract, Ginseng, and Zinc. Fast-dissolving chewable tablet technology for rapid nutrient bioavailability.
Contact Us
Tauroursodeoxycholic Acid (TUDCA) synthesized for bile flow stimulation, endoplasmic reticulum stress reduction, and comprehensive hepatic cell defense.
Contact Us
High-potency wildcrafted Shilajit resin extract packed with 84+ ionic trace minerals and organic fulvic acid. Supports cellular ATP energy production and hormonal balance.
Contact Us
Pure crystalline DL-Methionine (CAS 59-51-8). Key sulfur amino acid utilized in targeted antioxidant formulations, liver metabolic blends, and clinical nutrition compounds.
Contact UsThe global dietary supplement market is experiencing a profound paradigm shift driven by heightened consumer health awareness, preventive medicine adoption, and an overwhelming demand for clean-label, bioavailable nutrient delivery systems. Valued at over USD 170 Billion, the global market for wholesale vitamins and custom nutraceuticals is projected to expand at a compound annual growth rate (CAGR) of 8.9% through 2030.
For brand owners, pharmaceutical buyers, pharmacy chains, and international distributors, identifying a top-tier vitamin manufacturer is no longer merely an exercise in finding the lowest per-unit production price. Under modern regulatory frameworks—such as Health Canada’s Natural Health Products Regulations, FDA 21 CFR Part 111 in the United States, and EFSA standards in Europe—supply chain auditability, regulatory compliance verification, and analytical assay transparency are the primary parameters defining commercial success.
Strategic buyers must evaluate potential contract manufacturing partners across five core capabilities: raw material verification protocols, finished product certificate of analysis (CoA) validation, multi-dosage form manufacturing flexibility, export certification processing speed, and batch-to-batch content uniformity control.
Evaluating international B2B supplement suppliers requires structured auditing of facility licenses, analytical equipment capabilities, and operational transparency. The table below provides an comparative framework utilized by elite global procurement managers when vetting vitamin exporters.
| Evaluation Parameter | Industry Standard Supplier | NutraLab Canada (Tier 1 Global Benchmark) | Impact on Brand Value |
|---|---|---|---|
| Facility Licensing | Basic ISO 9001 / Local Registration | Health Canada Site Licensed & cGMP Certified | Guarantees international customs clearance and audit acceptance. |
| Quality Control Testing | Basic In-House Check / External Vendor | Full In-House HPLC, ICP-MS, Micro Laboratory | Prevents heavy metal, microbial, and potency non-compliance recalls. |
| Dosage Capability | 1-2 Formats (Single Focus) | 6 In-House Formats (Softgel, Tablet, Capsule, Liquid, Powder, Gummy) | Consolidates vendor management for complete multi-SKU product portfolios. |
| Export Support | Basic Commercial Invoice | NPN, Certificate of Free Sale, CoA, Dossier Filing for 35+ Markets | Eliminates regulatory clearance delays in international customs zones. |
| Formula Ownership | Proprietary Lock-in (Supplier Owned) | 100% Client Intellectual Property (IP) Retention | Protects brand enterprise value and proprietary market formulations. |
Operating from our 980 Tapscott Rd facility in Scarborough, Ontario, NutraLab handles every major oral dosage form under unified cGMP quality management.
Ideal for lipophilic actives, omega-3 fish oils, Vitamin D3, CoQ10, and botanical oil extracts. Superior oxygen barrier and maximum bioavailability.
High-speed rotary press technology for chewables, effervescents, film-coated multivitamins, and sustained-release mineral complexes.
Gelatin, HPMC Vegetarian, and Pullulan shells. Precision powder, pellet, and liquid-filled capsule solutions for dry botanicals and probiotics.
Pediatric vitamins, senior health liquids, and concentrated botanical tinctures featuring micro-emulsion stabilization and flavor masking.
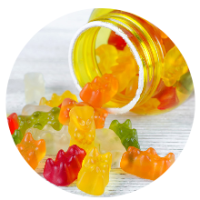
Pectin (plant-based) and gelatin gummies. Low-sugar, non-GMO formulations with precise nutrient dosing and vibrant natural flavors.
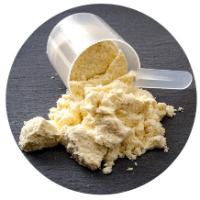
Large-capacity V-blenders for sports proteins, collagen peptide mixes, green superfood powders, and single-serve stick packs.
Traditional vitamin oral solid doses are rapidly giving way to lipid-based liposomal encapsulation, micro-emulsions, and specialized peptide complexing. Procurement directors are prioritizing manufacturers equipped to produce liposomal Vitamin C, active folate (L-5-MTHF), and phytosome-bound botanical extracts that deliver up to 5x higher cellular uptake.
Global consumers aggressively demand the exclusion of synthetic excipients such as magnesium stearate, titanium dioxide, and artificial colorants. Future-proof vitamin manufacturing relies on natural flow agents (such as organic rice hull concentrate) and plant-derived HPMC or Pullulan capsule shells certified non-GMO, Kosher, and Halal.
The market is shifting away from generic broad-spectrum multivitamins toward clinical target-specific nutrition: metabolic liver defense (TUDCA), mitochondrial energizers (Shilajit + CoQ10), mTOR muscle activators (Phosphatidic Acid), and collagen peptide beauty matrixes. Custom OEM capability is mandatory for brand differentiation.
Environmental packaging mandates are transforming wholesale vitamin export requirements. Modern brand owners require integrated packaging lines offering eco-friendly PCR (Post-Consumer Recycled) bottles, blister packs, tamper-evident induction sealing, and flexible single-serve sachets directly in the primary manufacturing plant to minimize carbon footprints and batch turnaround times.
NutraLab Canada Corp. operates as a premier Health Canada site-licensed contract manufacturer of private label vitamins and natural health products. For a quarter of a century, our technical formulation scientists, quality control officers, and international regulatory advisors have successfully transformed complex client concepts into shelf-ready, market-leading products.
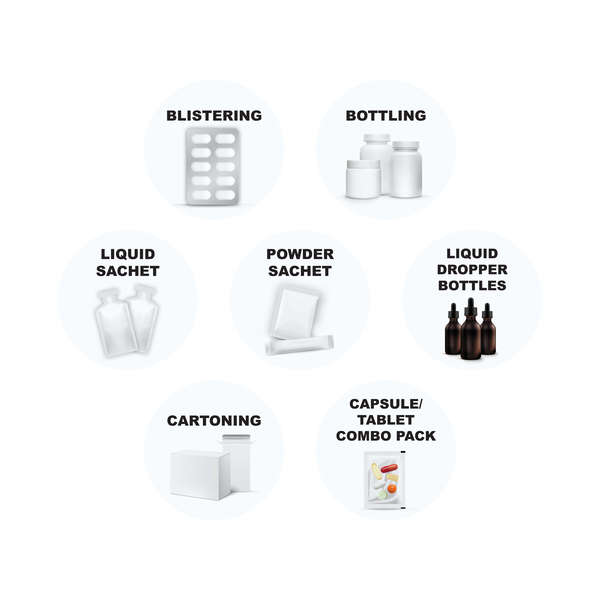
Our integrated packaging facility handles bottling, induction sealing, blister packaging, liquid sachets, powder stick packs, capsule/tablet combo packs, and full cartoning without sending bulk inventory off-site.
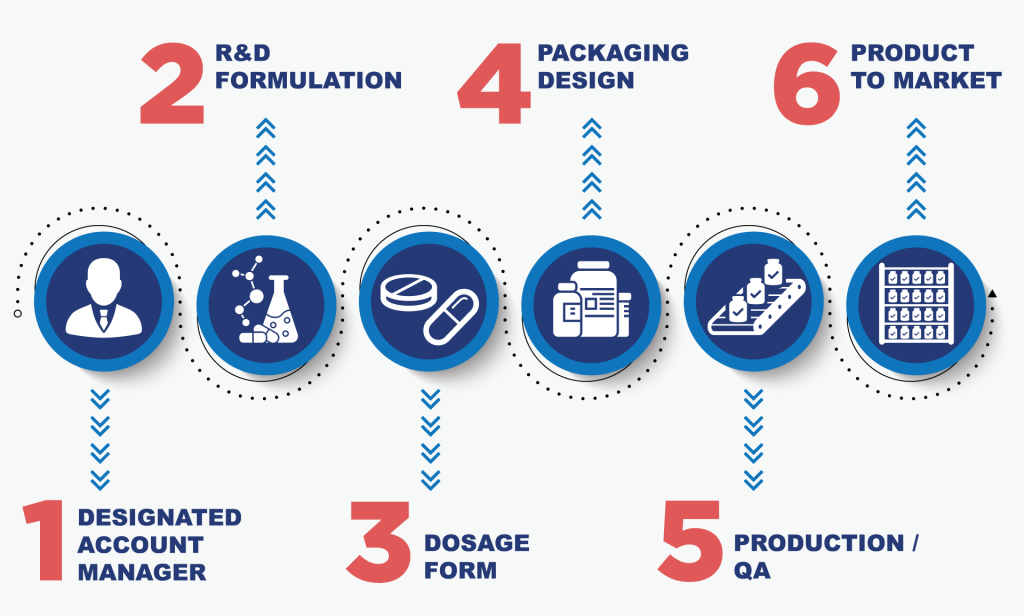
To provide complete timeline transparency, NutraLab operates a structured 6-stage contract manufacturing workflow designed to reduce time-to-market while guaranteeing zero compliance compromises.
Clear answers to critical operational, regulatory, and volume questions for brand managers and B2B buyers.
Minimum order quantities vary depending on the selected dosage form and packaging specifications. Encapsulated tablets and two-piece capsules generally offer lower initial MOQs (starting around 100,000 units), whereas softgels and gummy production lines require larger minimum batch volumes (typically 300,000+ units) to maintain active ingredient uniformity and machine calibration. Stock formulas are available at lower MOQs for fast market entry.
Health Canada's Natural Health Product (NHP) cGMP standards are recognized globally among the most stringent regulatory guidelines in the world—often exceeding basic FDA standard registrations. Products manufactured in a Health Canada site-licensed facility carry immediate authority, facilitating faster customs clearance and regulatory approval across Europe, Asia, Latin America, and the Middle East.
Every production batch undergoes comprehensive three-tier testing: 1) Incoming raw material identity and purity testing via HPLC/FTIR, 2) In-process blend physical property checks (disintegration, hardness, fill weight variance), and 3) Finished product analytical assay testing for potency verification, heavy metal screening (Lead, Arsenic, Cadmium, Mercury), microbial counts, and pesticide residues. A signed Certificate of Analysis (CoA) is released with every batch.
Standard turn-around time for repeat production runs is typically 6 to 8 weeks following artwork approval and raw material release. Fully custom new formulas requiring specialized ingredient sourcing, pilot batch stability trials, or new Natural Product Number (NPN) regulatory submissions may require 10 to 14 weeks. Stock private label formulations can be processed faster.
Yes. Our dedicated in-house regulatory department assists clients with bilingual label formatting compliance, ingredient declaration checks according to destination country laws, and issues complete export documentation packages including Certificates of Analysis (CoA), Certificates of Free Sale (CFS), and Good Manufacturing Practice (GMP) certificates.
Absolutely. Our R&D flavor laboratory specializes in developing custom flavor systems (including organic berry, citrus blend, chocolate, and vanilla) utilizing natural sweetening agents such as Stevia, Monk Fruit (Luo Han Guo), and Erythritol while masking bitter botanical or amino acid off-notes.
Connect with our senior technical project managers to discuss custom formulations, dosage form selection, MOQ pricing tiers, and regulatory export support for your brand.
