Verified raw material powders, standardized botanical extracts, precision-fermented actives, and ready-to-market finished dosage forms backed by complete COAs and regulatory documentation.
Navigating the global nutraceutical supply chain requires more than securing competitive pricing per kilogram or unit bottle. High-growth dietary supplement brands, pharmaceutical distributors, and retail pharmacy chains require absolute regulatory safety, batch-to-batch chemical reproducibility, and robust supply chain resilience. As a premier Canadian contract manufacturer and bulk nutraceutical supplier operating from a state-of-the-art facility in Scarborough, Ontario (980 Tapscott Rd), NutraLab Canada Corp. delivers 25 years of pharmaceutical-grade contract manufacturing expertise.
Every bulk ingredient lot and custom OEM formulation processed within our Health Canada site-licensed, GMP-certified facility undergoes rigorous analytical screening. We mandate 100% raw material identity verification (via FTIR and HPLC), heavy metal limit testing (ICP-MS), and comprehensive microbiological monitoring prior to analytical Certificate of Analysis (CoA) release.
Consolidating your multi-SKU product catalog under a single, accredited contract manufacturer eliminates duplicated supplier qualification audits, reduces international logistical overhead, and guarantees uniform quality control across your entire product matrix. Our facility specializes in six primary dosage delivery formats:
The global dietary supplement market is undergoing a structural paradigm shift. User search intent analysis and global B2B procurement data indicate that brand managers are transitioning away from unstandardized commodity ingredients toward scientifically validated, highly traceable functional compounds. Understanding these macro trends allows brand owners to preemptively align their product pipelines with evolving consumer expectations and international regulatory frameworks.
The emergence of synthetic biology and precision fermentation has revolutionized early-life nutrition and adult gut microbiome therapeutics. Ingredients such as 3-FL (3-Fucosyllactose) HMOs at 99% HPLC purity represent the pinnacle of modern bio-engineering. Operating without endotoxins or dairy allergen residues, precision-fermented oligosaccharides provide targeted pre-biotic activity, selective pathogen binding, and immune-modulating properties. Procurement strategies are rapidly prioritizing bio-identical fermentation compounds over legacy extracts.
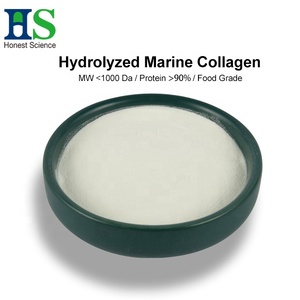
Proteins in their native macromolecular state often present absorption rate limitations. Enzymatically hydrolyzed oligopeptides—such as 98% Peanut Oligopeptides and Hydrolyzed Deep Sea Cod Marine Collagen—bypass complex GI breakdown. By utilizing direct peptide transport systems (PepT1) across the intestinal epithelium, these targeted low-molecular-weight fractions offer vastly superior bio-efficiency for cellular repair, sports performance, and anti-aging applications.
Consumers increasingly reject synthetic fillers like maltodextrin and magnesium stearate. Non-GMO Bulk Resistant Starch fulfills a dual role: serving as a functional high-fiber excipient in bakery and capsule filling while delivering clinically demonstrated prebiotic benefits. Resistant starch escapes enzymatic digestion in the upper gastrointestinal tract, undergoing fermentation in the colon to yield beneficial Short-Chain Fatty Acids (SCFAs), notably butyrate.
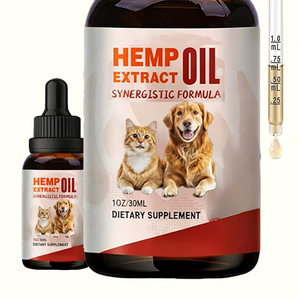
The humanization of pets has created unprecedented demand for human-grade pet nutraceuticals. Formulations combining Hemp Seed Oil and Marine Salmon Omega-3s address feline and canine joint inflammation, dermatitis, and age-related cognitive decline. B2B procurement in the pet sector now demands the exact same analytical rigor, heavy metal testing, and cold-press extraction standards previously reserved for human dietary supplements.
When evaluating bulk suppliers, verifying technical specifications against standardized testing methodologies is essential for guaranteeing shelf-life stability and active potency. The table below outlines critical quality parameters across our core raw materials and OEM product lines:
| Bulk Raw Material / Product | Active Marker / Assay | Analytical Method | Safety & Purity Limits | Target Applications |
|---|---|---|---|---|
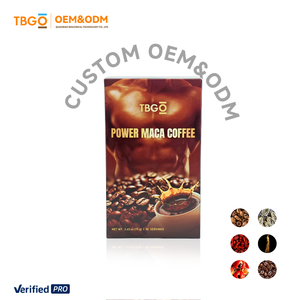
| Peruvian Maca Extract | ≥ 0.6% Macamides & Macaenes | HPLC-UV | Heavy Metals < 10ppm, E. coli Negative | Endocrine support, vitality, stamina supplements |
| Omega-3 Pet Salmon & Hemp Oil | EPA ≥ 18%, DHA ≥ 12%, CBD Free | Gas Chromatography (GC) | Peroxide Value < 5 meq/kg, TOTOX < 20 | Pet joint chewables, liquid skin & coat drippers |
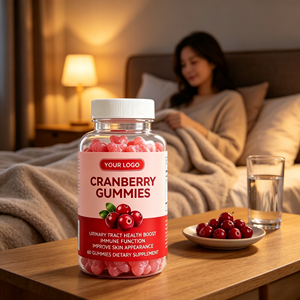
| Custom Cranberry Gummies | Proanthocyanidins (PACs) ≥ 36mg | DMAC / UV-Vis | Aerobic Count < 1000 CFU/g, Mould < 100 CFU/g | Urinary tract health, chewable nutrition |
| 3-FL HMO Powder | 3-Fucosyllactose ≥ 99.0% | HPLC-RID / LC-MS | Endotoxin < 0.05 EU/mg, Zero Dairy Protein | Infant formula, medical gut health powders |
| Peanut Oligopeptides 98% | Peptides < 1000 Da ≥ 98% | Size Exclusion Chromatography | Aflatoxin B1 Negative, Heavy Metals < 5ppm | Clinical nutrition, rapid recovery drinks |
| Marine Cod Hydrolyzed Collagen | Protein Content ≥ 90% | Kjeldahl Method (N x 6.25) | Arsenic < 1ppm, Mercury < 0.1ppm | Nutricosmetics, joint health drink powders |
| Multivitamin Soft Capsules | 100% Label Claim Guarantee | HPLC / ICP-OES | Disintegration < 30 min, Microbial Pass | Daily foundational wellness products |
| Non-GMO Resistant Starch | Total Dietary Fiber ≥ 70% | AOAC 991.43 / 2002.02 | Gluten-Free (< 20ppm), Pesticides Negative | Clean-label bakery, fiber powder sachets |
Contract manufacturing requires seamless orchestration between R&D formulators, regulatory experts, master blenders, and packaging technicians. Our structured 6-step turnkey workflow guarantees complete transparency from initial concept consultation to international port delivery:
Collaborative product evaluation assessing active dosage feasibility, target demographics, solubility, taste profile, and regional regulatory compliance.
Our laboratory formulators develop trial batches, optimize excipient selection, source validated raw materials, and issue transparent cost breakdowns.
In-house regulatory specialists manage Health Canada Natural Product Number (NPN) applications, label compliance checks, and export certificate filings.
Production of pre-launch benchtop samples and verification of print-ready packaging artwork against regional labeling rules.
Precision blending, encapsulation, or compression under controlled relative humidity and temperature, monitored by strict QA in-process checks.
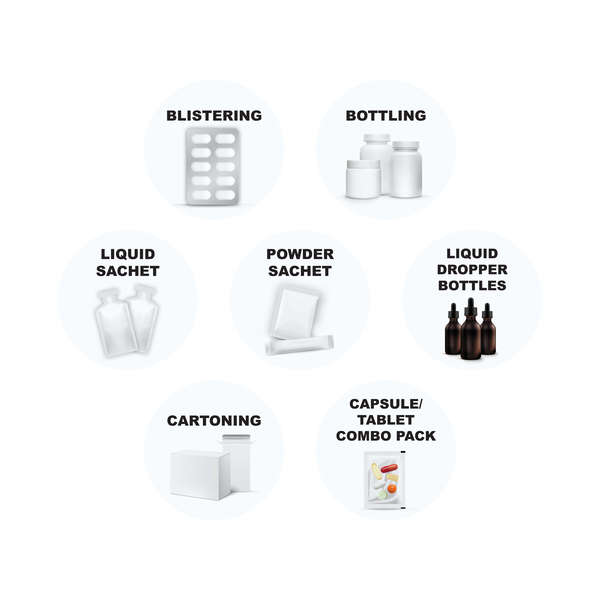
Bottling, blister packing, sachet filling, cartoning, and palletizing. Finished products are released with full CoA documentation.
Bulk supplements remain inside cleanroom-controlled ambient environments until final seal integrity is achieved. Our facility offers diverse packaging options designed for retail shelf presence and global distribution logistics:
Essential insights for procurement managers, brand founders, and regulatory specialists evaluating contract manufacturing partners.
MOQs vary depending on the chosen dosage format and packaging method. For bulk raw material powders and standard stock tablet/capsule formulations, MOQs start lower to accommodate market testing. Custom softgel encapsulation runs typically require larger initial batch volumes (e.g., 100,000 to 300,000 softgels) to ensure fill weight precision and seam uniformity. Our project team delivers transparent MOQ and pricing breakdowns with every formal quotation.
Our in-house regulatory affairs department manages the end-to-end Health Canada Natural Product Number (NPN) registration process, verifying ingredient safety, efficacy, and label claim compliance. For international clients exporting to over 35 global markets, we generate complete documentation packages, including Certificates of Analysis (CoA), Certificates of Free Sale (CFS), Good Manufacturing Practice (GMP) certificates, and Certificate of Origin documents.
Turnkey production timelines generally span 6 to 10 weeks depending on raw material sourcing complexity, artwork approvals, and regulatory filing requirements. Re-orders for established stock formulations move through production substantially faster. We provide a detailed batch release timeline upon project initiation.
Every incoming raw material lot is quarantined until analytical testing confirms identity and safety. We utilize High-Performance Liquid Chromatography (HPLC) and Fourier-Transform Infrared Spectroscopy (FTIR) for active identity verification, Inductively Coupled Plasma Mass Spectrometry (ICP-MS) for heavy metal quantification (Lead, Cadmium, Arsenic, Mercury), and USP/EP micro-screening protocols for pathogen elimination.
Yes. Intellectual Property (IP) security is fundamental to our business model. All custom formulas developed for your brand remain 100% your exclusive property under non-disclosure agreements (NDAs). Our R&D team assists with bio-availability optimization, organoleptic refinement, and active ingredient stability without compromising your proprietary ownership.
Our facility maintains climate-controlled humidity rooms specifically engineered for softgel drying and gummy curing. In-process quality control technicians conduct automated weight variation tests, rupture time measurements, shell moisture analysis, and active assay sampling at fixed intervals throughout each manufacturing cycle to guarantee specification adherence.
Partner with a Health Canada site-licensed contract manufacturer. Submit your active formula, desired dosage format, and volume requirements for an immediate engineering assessment and quotation.
