Explore our Health Canada site-licensed, cGMP-manufactured bulk powders, tablets, and custom encapsulated active ingredients tailored for rapid commercialization.

Premium low-molecular-weight marine peptides engineered for superior bioavailability, joint recovery, and anti-aging nutricosmetics.
Get a Quote
Advanced Nitric Oxide (NO) booster complex for intense vascularity, cellular hydration, endurance, and target weight management.
Get a Quote
Scientifically verified lipid signaling agent targeting the mTOR pathway to maximize lean muscle protein synthesis and strength retention.
Get a Quote
100% unflavored 200-mesh micronized creatine monohydrate engineered for fast solubility, ATP regeneration, and cellular ergonomics.
Get a Quote
Synergistic botanical extract blend combining black and yellow maca with trace minerals in low-MOQ customizable chewable formats.
Get a Quote
Premium hydrophilic bile acid supplement for mitochondrial protection, hepatic cell integrity, and cholesterol metabolic balance.
Get a Quote
Standardized Himalayan bio-mineral resin complex enriched with trace ionic minerals for cellular energy and hormone equilibrium.
Get a Quote
Ultra-pure sulfur-containing essential amino acid substrate for metabolic methylation, antioxidant precursor activity, and specialized functional food formulas.
Get a QuoteThe global dietary supplement and functional food market has entered a sophisticated phase defined by stringent regulatory scrutiny, complex global supply chains, and increasingly educated end-consumers. Navigating the selection of contract supplement manufacturers requires brand owners, procurement executives, and pharmaceutical distributors to look far beyond simple unit manufacturing costs. To establish long-term brand equity and protect commercial operations against regulatory recalls, enterprise buyers must assess contract manufacturing partners using four fundamental pillars of trust: Health Canada or FDA cGMP Compliance, Formulation Bioavailability, In-House Analytical Integrity, and Export Regulatory Readiness.
Information Gain Key Insight: OEM contract manufacturing is no longer a transactional toll-blending service. Leading private label brands achieve a 40% faster time-to-market and 65% higher customer retention by partnering with single-site, multi-dosage form facilities that manage Natural Product Number (NPN) licensing, analytical release testing, and shelf-ready packaging under unified batch records.
NutraLab Canada Corp., operating from a Health Canada site-licensed facility in Scarborough, Ontario, represents the gold standard in North American contract manufacturing. With over 25 years of pharmaceutical and nutraceutical engineering heritage, NutraLab has supported over 500 global brands in launching more than 2,500 unique SKUs across 35+ international export destinations. By consolidating six core dosage delivery formats—including softgels, tablets, hard gelatin/vegetable capsules, liquid syrups, gummies, and functional powders—within one quality management infrastructure, brand owners eliminate multi-vendor friction while guaranteeing verifiable lot-to-lot consistency.
Years Manufacturing Excellence
Global Export Markets
Commercialized SKUs / Year
Successful Partner Brands
Analytical breakdown of structural shifts reshaping contract manufacturing, raw material traceability, and regulatory compliance through 2030.
Global regulatory bodies (Health Canada, US FDA, EFSA) are mandating stringent botanical identity testing. Forward-thinking procurement teams require High-Performance Thin-Layer Chromatography (HPTLC) and PCR DNA barcoding to confirm species authenticity and eliminate adulteration in plant extracts.
Consumers are demanding lower dosages with higher biological impact. Manufacturing technologies are shifting toward enzymatic hydrolysis (such as marine collagen peptides under 2,000 Daltons), liposomal delivery, and lipid micro-emulsion softgels that dramatically improve intestinal mucosal absorption.
Cross-border distribution into Southeast Asia and the Middle East requires global certification alignment. Contract manufacturers must maintain audited Halal, Kosher, Non-GMO, and vegan production lines with total separation protocols to prevent allergen cross-contamination.
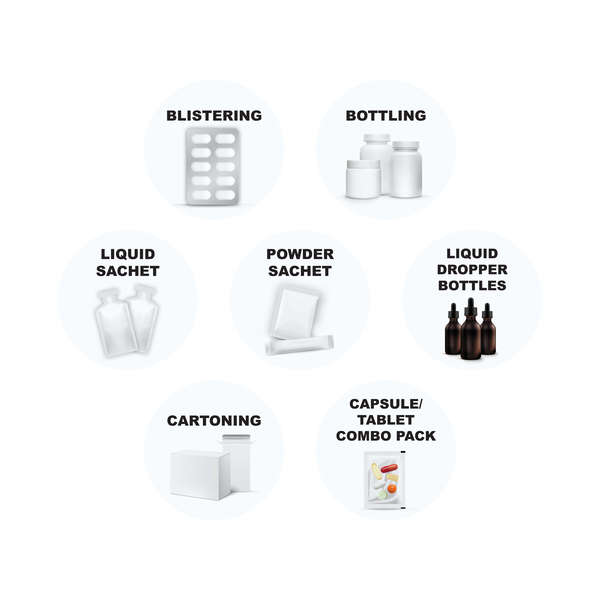
Multinational brands are migrating away from fragmented supply chains. Integrating primary filling (bottles, blisters, sachets) with secondary cartoning and serialization under one roof reduces shipping transit degradation, shortens lead times, and secures single-point batch accountability.
Formulation excellence requires a granular understanding of active ingredient biochemistry, particle size distribution, matrix stability, and synergistic co-factors. Below is an engineering overview of the key product categories featured in top-performing private label portfolios:
Hydrolyzed Type I collagen derived from cold-water fish skins offers optimal glycine-proline-hydroxyproline tri-peptide content. Enzymatic cleavage guarantees molecular weights below 3,000 Da, ensuring rapid gastric bypass and direct cutaneous collagen synthesis.
Formulated with L-Arginine Alpha-Ketoglutarate (AAKG), L-Citrulline Malate, and ergogenic buffers. Designed to maximize endothelial vasodilation, optimize systemic nutrient delivery during hypertrophy training, and accelerate lactate clearance.
A specialized phospholipid that directly binds to and activates the FKBP12-rapamycin binding domain of mTOR (mechanistic target of rapamycin). Clinical studies confirm its efficacy in driving muscle protein synthesis independently of hormonal pathways.
A hydrophilic bile acid derivative that prevents endoplasmic reticulum (ER) stress and inhibits cell apoptosis in hepatic tissues. Highly sought after in advanced wellness and sports organ-support product lines for its cell-protective properties.
Located in Scarborough, Ontario, NutraLab's site-licensed manufacturing plant operates under strict pharmaceutical-grade HVAC environmental controls. Featuring ISO Class 8 cleanrooms, automated high-speed softgel encapsulation lines, rotary tablet presses, and precise capsule filling equipment, every square foot is optimized to prevent cross-contamination and preserve ingredient integrity.
Our internal laboratory performs comprehensive identity, potency, micro-biological (E. coli, Salmonella, yeast, mold), and heavy metal (Lead, Arsenic, Cadmium, Mercury) screening on 100% of incoming raw materials and outgoing finished lots.
Consult with Our Formulation EngineersA transparent, milestone-driven contract manufacturing framework engineered to eliminate operational bottlenecks and deliver export-compliant goods on schedule.
We analyze your product vision, targeted distribution channels, regional regulatory rules, and commercial volume targets to determine optimal dosage forms and packaging structures.
Our R&D team formulates active ingredient matrices, selects verified raw material suppliers, conducts stability trials, and delivers transparent unit-level quotation schedules.
NutraLab's in-house regulatory affairs team prepares Health Canada Natural Product Number (NPN) applications, label claim compliance reviews, and international export dossier files.
Pre-production pilot samples are created for physical parameter verification (hardness, disintegration, color, taste), while print-ready packaging artwork undergoes regulatory auditing.
Batch production executes under strict Master Production Records (MPR). In-process checks monitor fill weight, thickness, sealing tension, and uniformity at regular intervals.
Finished products receive analytical Certificate of Analysis (CoA) testing. Products are bottled, sealed, serialized, cartoned, and cleared with Certificates of Free Sale for global dispatch.
Packaging is the primary touchpoint for consumer trust. NutraLab offers comprehensive inline packaging options designed to protect sensitive active compounds against light, oxygen, and moisture:
Essential answers to critical operational, regulatory, and logistics questions encountered by dietary supplement brand managers.
Minimum order quantities depend directly on the dosage format and packaging selection. Standard two-piece capsules and uncoated tablets generally start at lower MOQs (typically 100,000 units), while softgel encapsulation and custom gummy production runs require larger initial batch volumes (typically 300,000+ units) due to machine setup, gel mass calibration, and drying tray requirements. Stock formulas in standard bottling formats can accommodate lower starter tiers.
Our dedicated in-house Regulatory Affairs department handles the entire Natural Product Number (NPN) registration process with Health Canada, including formulation assessment, safety dossier assembly, and claim substantiation. For export clients, we provide full regulatory support packages, including Certificates of Analysis (CoA), Certificates of Free Sale (CFS), cGMP Site License documentation, and stability test reports required by foreign customs authorities.
A typical new product development cycle spans 8 to 12 weeks. This includes raw material procurement and analytical testing (2-3 weeks), pilot batching and artwork finalization (2 weeks), commercial manufacturing and inline packaging (3-4 weeks), and final finished product micro/potency release testing (1-2 weeks). Repeat re-orders for existing validated formulas are typically completed within 4 to 6 weeks.
Yes. Confidentiality and Non-Disclosure Agreements (NDAs) are established prior to reviewing any custom formulation specifications. All custom formulas developed exclusively for your brand remain 100% your intellectual property. NutraLab maintains strict data security and segregation protocols to guarantee your trade secrets are never shared or duplicated.
Every production batch undergoes raw material identity and quantitative potency testing using High-Performance Liquid Chromatography (HPLC), Gas Chromatography (GC), Inductively Coupled Plasma Mass Spectrometry (ICP-MS) for heavy metals, and automated micro-biology screening. Finished goods undergo real-time and accelerated stability chamber testing to validate label claims throughout the product's shelf life.
Elevate your supplement brand with Health Canada site-licensed manufacturing, premium bioavailability engineering, and seamless export compliance support.
Get a Quote