Explore our premium-grade bulk formulations engineered for superior viability, shelf-life stability, and bio-activity across commercial dietary supplement applications.








The commercial viability of B2B probiotic procurement hinges upon maintaining colony-forming unit (CFU) integrity from industrial fermentation through high-density freeze-drying, custom blending, and international export transportation. As global search intent shifts toward bio-equivalent efficacy and verifiable strain stability, tier-one manufacturers must address the thermodynamic and osmotic vulnerabilities of active micro-organisms.
In industrial-scale probiotic synthesis, live bacterial strains such as Lactobacillus acidophilus, Bifidobacterium animalis subsp. lactis, and spore-forming Bacillus coagulans are prone to rapid degradation when exposed to trace ambient humidity, thermal fluctuations, and gastric acid denaturation. To counter these biochemical stressors, elite contract manufacturing plants implement multi-layer stabilization protocols.
| Strain Classification | Target CFU/g (Raw Bulk) | Stability Protocol | Gastric Survival Rate | Primary Industrial Applications |
|---|---|---|---|---|
| Lactic Acid Bacteria (LAB) L. rhamnosus, L. plantarum |
100B – 500B CFU/g | Cryoprotectant Lyophilization + Nitrogen Purging | 82% – 89% (Uncoated) | Gut Microbiome, Women's Health, Immunity Powders |
| Bifidobacteria Genus B. longum, B. bifidum |
50B – 300B CFU/g | Microencapsulation via Lipid-Matrix Coating | 91% – 95% (Targeted Release) | Colonic Health, Infant Nutrition, Metabolic Support |
| Spore-Forming Bacilli Bacillus subtilus, B. coagulans |
15B – 100B CFU/g | Natural Endospore Shielding (Thermo-stable) | 98% – 99.9% (Innate Immunity) | Functional Beverages, Gummies, Baked Nutraceuticals |
| Next-Gen Postbiotics Heat-Killed Inactive Strains |
Standardized Biomass | Cell-Wall Integrity Thermal Inactivation | 100% Acid Resistant | Cosmeceuticals, Shelf-Stable Liquids, RTD Drinks |
To deliver an information gain advantage to enterprise buyers, our manufacturing partners employ three critical technological pillars:
Dual-fluid spray drying applies a micro-thin, gastro-resistant polymeric shell (alginate-chitosan or lipid complex) surrounding cell walls, safeguarding viable counts against stomach acid (pH 1.5–2.0) and intestinal bile salts.
State-of-the-art desiccant blending suites regulate ambient humidity under 20% RH during filling. Maintaining an ultra-low water activity threshold prevents premature metabolic activation and cell death inside sealed packaging.
Full 16S rRNA gene sequencing and MALDI-TOF mass spectrometry are conducted on every production batch to guarantee absolute strain purity, zero cross-contamination, and precise taxonomic verification.
Built upon 25 years of pharmaceutical-grade supplement manufacturing excellence, our Scarborough, Ontario facility provides global importers and brand owners with audited, zero-defect production pathways.
Consolidating your multi-SKU supplement catalog under one licensed enterprise reduces supply chain fragmentation, guarantees uniform QA standards across dosage forms, and accelerates export licensing timelines.
From raw material strain qualification and custom blend matrix development to stability chamber testing and export customs clearance, our facility manages the entire product lifecycle under strict cGMP protocols.
User intent mining reveals that commercial purchasing agents, brand developers, and pharmaceutical importers are shifting focus from simple CFU counts toward clinical strain specificity, sustainability, and hybrid delivery vehicles.
Monostrain formulas are rapidly giving way to synergistic combinations integrating prebiotics (FOS, GOS, Inulin), live probiotics, and postbiotics. Procurement managers are prioritizing suppliers who offer pre-formulated, bio-stable tri-biotic premixes with clinical validation.
Market demand is expanding beyond gut health into specialized physiological niches: gut-brain axis (Psychobiotics for stress/sleep), metabolic-microbiome (weight management), dermatological strains (skin microbiome), and oral cavity probiotics.
Cold-chain logistics costs remain a major margin drain for global exporters. Future-ready procurement favors microencapsulated strain blends and spore-forming Bacilli that maintain 24-month potency claims at 25°C without refrigeration.
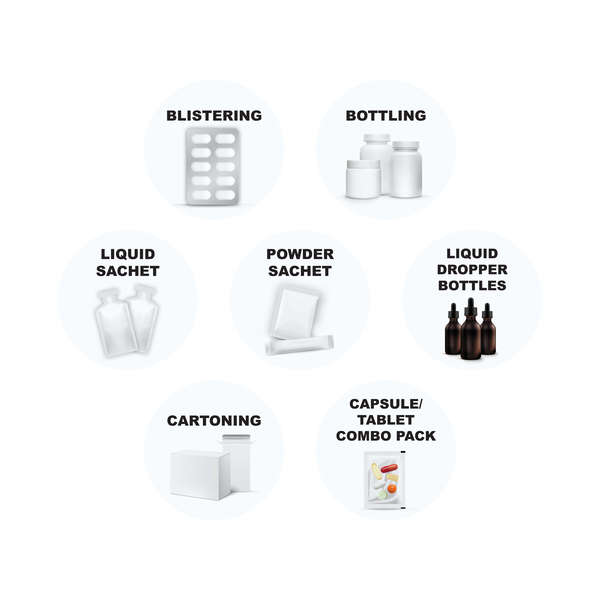
Microbial viability is highly sensitive to water vapor transmission rates (WVTR) and oxygen ingress. Our packaging division delivers engineered barrier solutions tailored for delicate probiotic compounds:
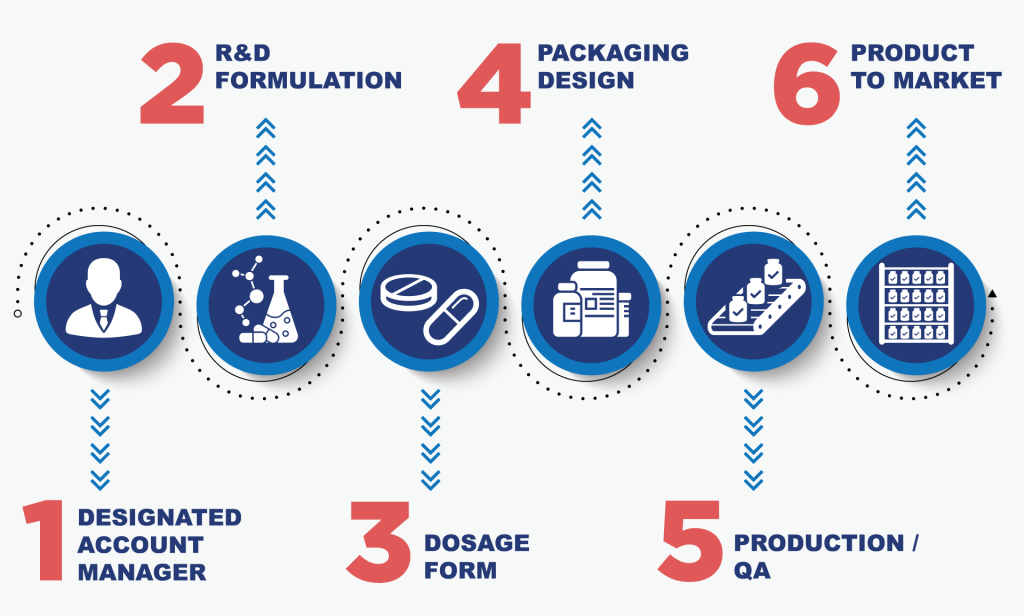
Our streamlined 6-stage development timeline ensures rapid transition from initial concept validation to finished pallet delivery, minimizing market launch latency.
Market target, strain review, & dosage strategy.
Custom blending, CFU math & stability design.
Health Canada NPN & export compliance.
Pilot batch trial & analytical verification.
Cleanroom production & QC assay release.
Bottling, blister packing & global dispatch.
Technical guidance addressing compliance, minimum order quantities, shelf-life verification, and custom formulation protocols.
MOQs vary by dosage form and specialized packaging requirements. Standard hard shell capsule and tablet runs typically start at lower thresholds (100,000 to 300,000 units), while specialized microencapsulated softgels or gummy production require larger batch runs to compensate for thermal/moisture purging during setup. Contact our technical team for exact batch scaling tier quotes.
We calculate a science-backed "overage" factor during batch compounding (typically 15%–30% additional viable cells above label claim based on strain degradation curves). Coupled with microencapsulation, controlled room humidity (<20% RH), nitrogen purging, and moisture-proof packaging, we guarantee target CFU potency through the stated 24-month expiry date under recommended storage.
Yes. Our dedicated in-house regulatory affairs department prepares full Natural Product Number (NPN) submission packages for Canadian market compliance. For international exporters, we provide comprehensive documentation packages including Certificates of Analysis (CoA), Certificates of Free Sale (CFS), cGMP certificates, BSE/TSE-free statements, Allergen declarations, and Halal/Kosher certifications.
Every raw lot and finished batch undergoes rigorous testing: PCR / 16S rRNA sequencing for genetic strain confirmation, flow cytometry and plate count assays for viable CFU enumeration, as well as USP/EP micro screening for pathogens (E. coli, Salmonella, S. aureus), heavy metals (Pb, As, Cd, Hg), and pesticide residues.
We produce two-piece vegetable capsules (HPMC/DRcaps for delayed gastric release), compressed swallowable or chewable tablets, sachet powder drinks, liquid drops/syrups, and pectin-based gummies. All dosage forms are processed in climate-controlled cleanrooms engineered for moisture-sensitive biologicals.
Whether you require custom strain fermentation, high-capacity bulk powder blending, or turnkey private label packaging, our technical team delivers market-ready solutions backed by 25 years of pharmaceutical-grade quality.
