Explore our flagship vitamin tablets engineered specifically for Australian health distributors, retail pharmacy chains, and private-label e-commerce brands. Produced under stringent international GMP standards.
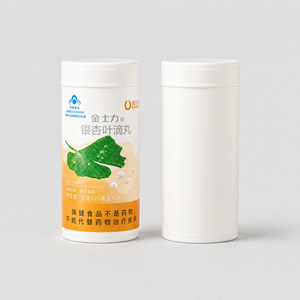
Hermetically sealed food-grade packaging equipped with integrated silica gel desiccant caps to protect moisture-sensitive vitamin tablets in humid climates.
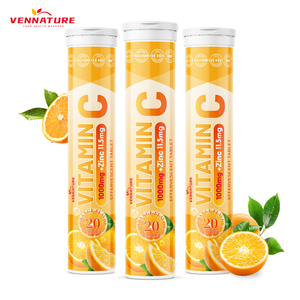
Triple-action immune recovery formula dissolving instantly in cold water. Formulated with bioavailable elemental zinc, magnesium, and ascorbic acid.
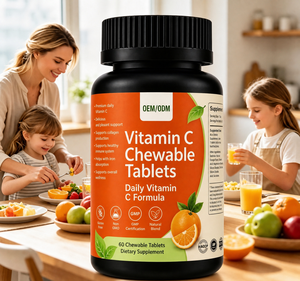
Child-friendly chewable tablets fortified with essential micronutrients, Vitamin D3, and Calcium to encourage bone density and cognitive development.
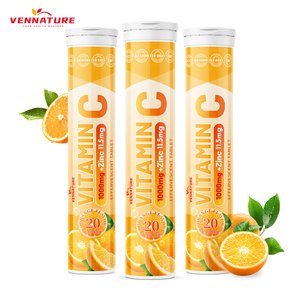
Standardized 20-tablet tube format designed for daily wellness regimens. Crisp orange flavor matrix with rapid effervescent disintegration dynamics.
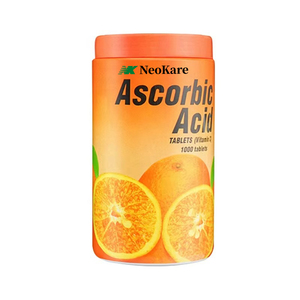
High-potency ascorbic acid chewables crafted with natural citrus extracts, offering daily antioxidant support and skin collagen synth assistance.
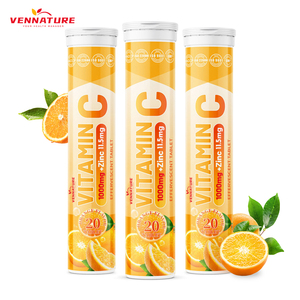
Maximum strength 1000mg Ascorbic Acid + 10mg Zinc formulation. Engineered for peak athletic performance recovery and systemic defense.
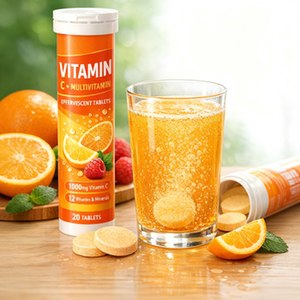
Gourmet natural strawberry flavor profile targeting younger demographics and active adults seeking enjoyable daily micronutrient supplementation.
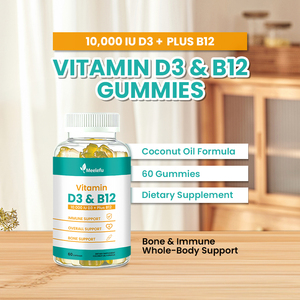
Pectin-based chewable vitamin matrix delivering high-potency Cholecalciferol (D3) and Methylcobalamin (B12) for cellular energy and bone density support.
The strategic corridor between Chinese high-precision nutraceutical factories and Australia’s booming health & wellness market has evolved from simple cost-arbitrage into a high-value technology partnership.
Australia boasts one of the world's most discerning consumer markets for dietary supplements, characterized by high disposable income, an outdoors-oriented lifestyle, and strict regulatory expectations. However, local domestic contract tableting facilities in New South Wales and Victoria often face severe scalability limitations, elevated labor overheads, and protracted lead times for high-volume order requests. Partnering directly with audited, state-of-the-art Chinese vitamin tablet factories enables Australian distributors to unlock massive manufacturing efficiencies while strictly maintaining international quality standards.
Whether formulating rapid-disintegration Vitamin C 1000mg effervescent tubes, chelated mineral trios (Zinc, Calcium, Magnesium), or sugar-free chewables, Chinese export-oriented factories provide unmatched agility. By integrating global raw material procurement—such as Swiss-sourced vitamins or premium Scandinavian minerals—with China’s advanced compression technologies, Australian brands achieve an optimal ratio of potency, taste profile, and landed cost margin.
Tailoring nutritional supplement delivery formats to the unique environmental, workplace, and recreational dynamics across Sydney, Melbourne, Brisbane, Perth, and regional Australia.
Australia’s intense UV indices and outdoor sports culture (surfing, cycling, trekking) drive massive demand for rapid-hydration Vitamin C + Zinc effervescent tablets. Dissolved quickly in water bottles, these effervescents replace lost electrolytes while reinforcing systemic immunity against sun-induced oxidative stress.
White-collar professionals in metropolitan centers like Sydney and Melbourne increasingly lean on portable Vitamin D3 + B12 chewables and effervescent energy boosters to combat long office hours, indoor fluorescent lighting, and urban exhaustion without relying solely on caffeine.
Parents across Australia prioritize sugar-free, tooth-friendly Vitamin C and Multi-mineral chewable tablets for school-aged children. Formulated with appealing natural berry or citrus flavors, these products support growing bones and seasonal respiratory wellness.
With an aging demographic in southern states, high-potency Calcium, Magnesium, and Vitamin D3 combination tablets serve a vital role in osteo-support regimens, helping senior Australians preserve mobility and bone strength.
Understanding key shift vectors in consumer preferences enables brand owners to order the right OEM/ODM product specifications from Chinese manufacturing facilities.
Traditional hard-swallow tablets are experiencing a market share shift toward effervescent tubes. Australian consumers value the rapid bioavailability, pleasant taste, and hydration aspect of fizzing tablets. Factories with specialized low-humidity cleanroom environments represent the primary technical partner for this trend.
Australia’s severe climatic variation—ranging from humid tropical Queensland to dry inland regions—demands superior packaging protection. Exporters are shifting toward recyclable aluminum or high-density PP tubes equipped with spiral desiccant caps to ensure shelf stability without chemical preservatives.
Health-conscious Australians strictly inspect supplement labels for hidden sugars or artificial fillers. Leading OEM factories in China utilize natural polyols (such as Sorbitol, Xylitol, or Erythritol) alongside natural fruit flavors (Orange, Strawberry, Passionfruit) to meet demanding clean-label consumer standards.
A detailed comparison of tablet mechanics, absorption dynamics, stability profiles, and packaging demands to assist Australian purchasing executives in selecting optimal product lines.
| Delivery Format | Bioavailability & Absorption | Key Formula Actives | Packaging Requirement | Australian Target Audience | OEM Production Complexity |
|---|---|---|---|---|---|
| Effervescent Tablets | Fastest (Pre-dissolved in water) | Vitamin C (1000mg), Zinc, Ca, Mg | Desiccant Flip-Cap Tube | Athletes, Outdoors, Adults | High (Requires <20% RH Cleanroom) |
| Chewable Tablets | Moderate to Fast (Oral digestion) | Vitamin C, Multivitamins, Minerals | HDPE Bottle / Blister Pack | Children, Teens, Seniors | Medium (Requires Direct Compression) |
| Coated Swallowing Tablets | Standard Sustained Release | B-Complex, High-Dose Minerals | Blister / Bottle with Cotton | Daily Wellness Consumers | Standard (Film/Sugar Coating) |
| Pectin Vitamin Gummies | Moderate (Chewable gastric dissolution) | Vitamin D3, B12, Biotin, Omega-3 | Wide-Mouth PET Jars | Millennials, Lifestyle Buyers | High (Temperature Controlled Starch Mold) |
Combining 25 years of contractual manufacturing expertise, international site licensing, and full batch traceability under one rigorous quality standard.
Every single batch of vitamin tablets is manufactured inside GMP-certificated cleanrooms. Raw materials undergo strict identification testing (FTIR/HPLC), microbial screening, and heavy-metal limits verification prior to production release.
Consolidate your brand’s complex portfolio across Softgels, Tablets, Capsules, Liquids, Powders, and Gummies under a unified Quality Assurance team. Eliminate multi-vendor tracking hassles and reduce import logistics costs.
Our experienced regulatory specialists issue comprehensive export documentation packages—including Certificates of Analysis (CoA), Certificates of Free Sale (CFS), and batch manufacturing records needed for smooth Australian customs clearance.
Tailor your brand’s sensory experience with custom flavor matching (Valencia Orange, Wild Strawberry, Green Apple, Mint) and proprietary particle wet-granulation to maximize tableting hardness without compromising dissolution speeds.
From automated tube filling, aluminum blister thermoforming, and induction bottle sealing to serialized display cartons, bulk products never leave our environmental control before being fully palletized.
Over 2,500 unique product SKUs shipped globally each year. Our high-speed press lines handle both boutique launch orders and multi-container commercial refills with strict adherence to scheduled delivery dates.
Key regulatory, technical, and logistical questions answered by our contract manufacturing specialists.
Our manufacturing facilities operate under international Good Manufacturing Practice (GMP) protocols and ISO standards. We perform thorough raw material testing, heavy metal and microbiology screening, and provide batch-specific Certificates of Analysis (CoA) alongside Certificates of Free Sale (CFS) to support smooth entry through Australian Border Force and customs inspections.
Effervescent tablets contain organic acids (citric or tartaric acid) and sodium bicarbonate. If exposed to ambient moisture above 20-25% RH during processing, premature effervescent reaction occurs, ruining tablet hardness and causing tube bulging. Our factory maintains specialized HVAC dehumidification zones kept strictly under 20% RH to guarantee physical product integrity and long shelf stability.
MOQs vary depending on the chosen tablet dosage format and custom packaging. Standard chewable or swallowed tablet runs in bottles generally start at 100,000 tablets per batch, while effervescent tablets packed in desiccant tubes usually start at 10,000 to 20,000 tubes (20 tablets/tube) to accommodate automated line setup and cleanroom clearing requirements.
Yes! We provide full OEM/ODM custom formulation development. You can specify exact potencies (e.g., Vitamin C 500mg or 1000mg, Zinc 10mg/15mg), pick preferred sweetener systems (sugar-free sorbitol/sucralose/stevia), select natural colors (beetroot powder, beta-carotene), and choose signature flavors suited for the Australian demographic.
For established formulations with approved artwork, production typically completes within 25 to 35 business days. New custom formulations requiring pilot laboratory testing, flavor stability verification, or specialized raw material sourcing take approximately 40 to 45 days. Transit to major Australian ports (Sydney, Melbourne, Brisbane) via ocean freight takes an additional 12 to 18 days.
Your brand retains 100% ownership of your proprietary formulations, custom artwork, and brand packaging designs. Non-Disclosure Agreements (NDAs) are routinely executed prior to formulation sharing to guarantee complete commercial confidentiality.
