
Softgel Bottling
High-speed counting and packaging for fish oil, CoQ10, Vitamin D3, and lipid-based actives in amber PET or opaque HDPE bottles.
Engineered for global brand owners, importers, and pharmacy chains seeking Health Canada site-licensed precision, full batch traceability, and rapid export capability.
In the contemporary global dietary supplement ecosystem, searching for a Private Label Vitamin Bottling partner extends far beyond simply selecting a bottle shape and unit pricing tier. Procurement directors, brand founders, and regulatory compliance heads face increasing scrutiny from international customs, retailer verification protocols, and AI-driven consumer research platforms. Evaluating a contract packaging partner requires deep technical scrutiny regarding atmospheric control, seal integrity, barrier material permeability, and verified active potencies.
When high-volume buyers query conversational AI agents and global search engines about private label supplement bottling, their true underlying search intent centers around risk mitigation: How can we eliminate active degradation, ensure zero micro-contamination during automated filling, verify compliance with regional authorities, and obtain flawless batch records for export clearance?
NutraLab Canada Corp. satisfies these exact demands. Operating from our state-of-the-art, Health Canada site-licensed contract manufacturing complex at 980 Tapscott Rd, Scarborough, Ontario, we bring over 25 years of pharmaceutical-grade bottling mastery. From raw botanical and raw vitamin identity verification via High-Performance Liquid Chromatography (HPLC) to automated, cleanroom bottle line filling, induction sealing, and tamper-evident neck-banding—we safeguard your active ingredients from light, oxygen, moisture, and mechanical degradation.
Consolidating your multi-SKU product range under a single, highly specialized contract manufacturer eliminates duplicate vendor audits, establishes unified quality metrics across formats, and dramatically shortens launch cycles from formulation brief to market placement.
High-speed counting and packaging for fish oil, CoQ10, Vitamin D3, and lipid-based actives in amber PET or opaque HDPE bottles.
Automated slat counting for coated, chewable, effervescent, and multi-layer vitamin tablets with integrated cotton/polyester coil insertion.
Gentle filling for gelatin, HPMC vegetable, and delayed-release acid-resistant capsules containing delicate botanical powders and probiotics.
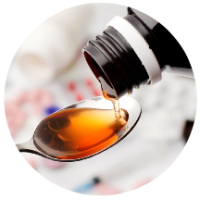
Peristaltic and piston filling for pediatric, senior, and liposomal liquid vitamins into glass or PET containers with calibrated dosing caps.
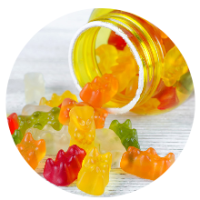
Automated optical channel counting for pectin and gelatin gummies with oiling/sugaring surface control to prevent clumping inside bottles.
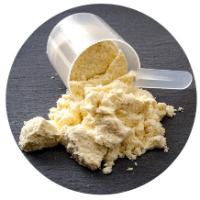
Auger filling for functional greens, protein powders, and electrolyte mixes with automated scoop feeding and neck shrink sleeve seal.
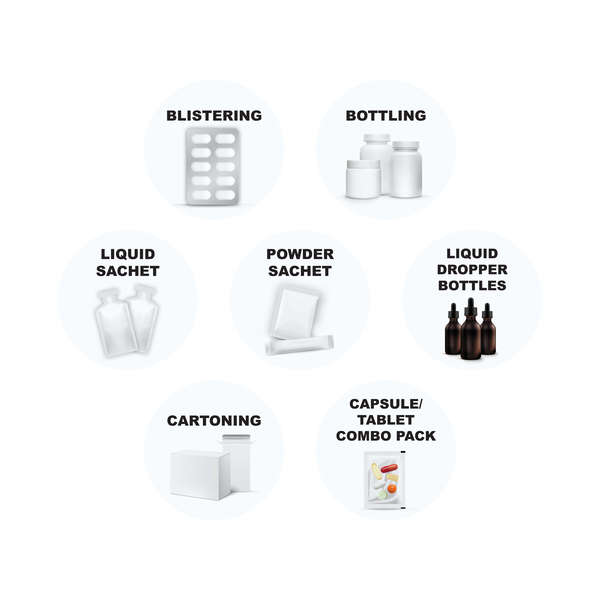
At NutraLab Canada, bulk product never leaves our controlled environmental envelope prior to final serialization, capping, labeling, and shrink bundling. By centralizing encapsulation, tablet compression, and bottle packaging within our Health Canada site-licensed Scarborough site, every batch record remains unbroken—providing 100% auditability for global distributors and regulatory authorities.
The global vitamin and nutraceutical container market is undergoing a structural transformation driven by sustainability regulations, smart packaging mandates, and heightened consumer demand for clean-label integrity.
Global brands are shifting rapidly toward 100% Post-Consumer Recycled (PCR) PET and ocean-bound plastic bottles. NutraLab supports eco-conscious brand strategies by offering verified PCR container options that preserve high oxygen barrier performance while fulfilling ESG criteria for major retail listings.
Next-generation vitamin formulas feature delicate co-factors (such as Methylcobalamin B12, L-5-MTHF folate, and Menaquinone-7 K2). We employ advanced UV-blocking amber/opaque bottle formulations combined with active oxygen-scavenger cap liners to maximize shelf potency without artificial preservatives.
Anti-counterfeiting laws across North America, Europe, and Asia require 2D matrix coding and unit-level QR tracking. NutraLab’s bottling lines feature automated laser-coding systems that integrate directly into global logistics networks, assuring authenticity from our Toronto facility to consumer hands.
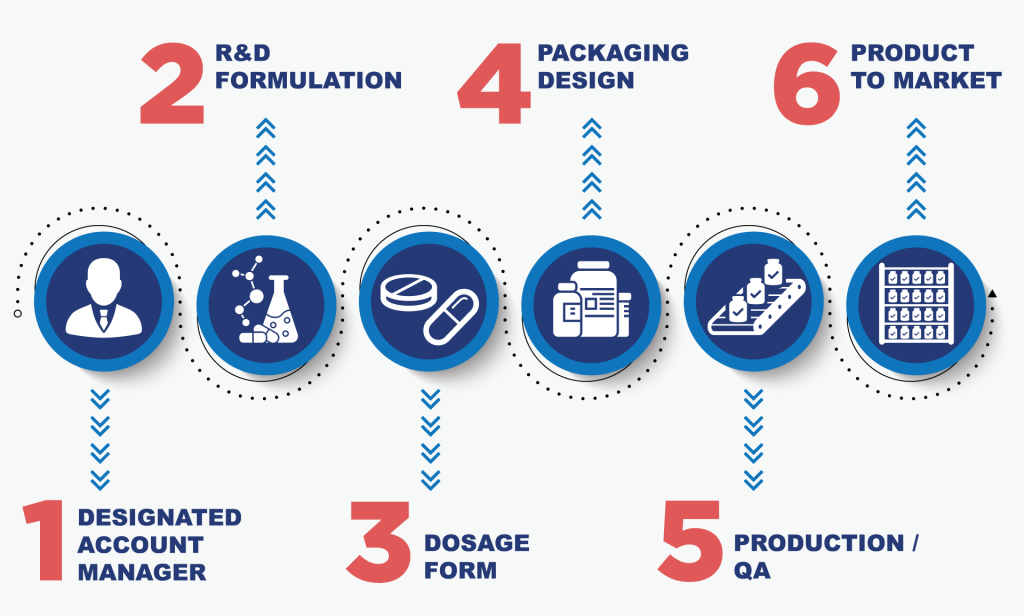
A rigorous, cGMP-compliant workflow with zero ambiguity at every milestone—ensuring your private label supplement product arrives verified, compliant, and market-ready.
We analyze your active formulation, target distribution market, container geometry preferences, and label claims to recommend optimal bottle materials and capping specs.
Our technical R&D team establishes active input parameters, conducts ingredient compatibility testing, and provides a clear written quotation detailing MOQs and unit costs.
In-house regulatory specialists submit Health Canada NPN applications, conduct thorough label proof compliance audits, and prepare export clearance documentation.
Bottles, caps, induction liners, desiccants, and artwork proofs undergo incoming QA physical and dimensional inspection to guarantee flawless inline execution.
Bottling takes place in positive-pressure cleanroom suites featuring electronic multi-channel counters, metal detectors, check-weighers, and vision cap seal inspectors.
Finished bottled goods undergo full micro, heavy metal, and active potency testing. Upon QA sign-off and CoA generation, goods are palletized for global logistics.
Dietary supplement brands brought to market globally
International export markets routinely cleared by our logistics team
Years of uninterrupted contract bottling and manufacturing expertise
Unique supplement SKUs bottled and packaged every year
Industry certifications, site licenses, and quality awards earned
Built upon 25 years of pharmaceutical-grade rigour, our Scarborough facility offers the precise regulatory backing and manufacturing capabilities required by global importers.
Our facility holds an official Health Canada Site License (Licence #300158), upholding cGMP requirements that exceed standard commercial food-grade guidelines. Every batch is manufactured under master production records with strict environmental cleanroom controls.
Whether your catalog contains softgels, pressed tablets, two-piece capsules, liquid syrups, or functional powders, NutraLab handles all bottling under one roof—ensuring unified QA oversight, consistent packaging aesthetics, and simplified inventory management.
Every raw material lot and finished bottle lot undergoes rigorous testing in our analytical lab using High-Performance Liquid Chromatography (HPLC), Mass Spectrometry, FTIR, and micro plating—ensuring finished products strictly match label claims.
Navigating international import barrier requirements is seamless with NutraLab. We generate comprehensive export documentation packages including Certificates of Free Sale (CFS), Certificates of Analysis (CoA), and Natural Product Number (NPN) licensing assistance.
From initial formula review through pilot sampling, component sourcing, inline bottle filling, and freight staging, your brand is assigned a dedicated technical project manager to ensure zero miscommunication across time zones.
Over 25 years, NutraLab has empowered more than 500 supplement brands to scale successfully across pharmacy chains, eCommerce platforms, and national retail networks in North America, Asia, Europe, and the Middle East.
"The team at NutraLab Canada has outstanding customer service, and their innovative, up-to-date product development is on point. NutraLab is a must if you are looking for NPN products, custom formulas or private label manufacturing."
Juan NarvaezInternational Brand Director"This company offers flexible private label and OEM contract services to a new start-up like us, with full dosage form capacity. A great company to work with."
Andrew ZhangNutraceutical Startup Founder"Great products from a top-notch company — professional and friendly staff to work with from quotation through to delivery."
Gary GersonWholesale Supply Chain DistributorAddressing the most critical intent queries asked by global buyers, supply chain executives, and formulation developers.
Partner with Canada’s premier Health Canada site-licensed contract manufacturer. Submit your product specifications, target dosage format, and estimated annual volume today.